
BELT CONVEYORS
Belt Conveyor Systems from a Trusted Warehouse Supplier & Integrator
We design, supply, and install belt conveyor systems that move your products faster, farther, and more reliably — from flat transport to steep inclines, light parcels to heavy loads, across every inch of your warehouse.
Speak with an expert  515-635-1555
Home / Warehouse Equipment / Conveyors and Automated Systems / Belt Conveyor System
Belt Conveyor Systems
Belt conveyor systems are one of the most widely used solutions in warehouse automation, moving packages, cartons, and bulk materials efficiently from point A to point B across distribution, fulfillment, and manufacturing operations.
At Midwest Warehouse Solutions (MWS), we are a full-service belt conveyor supplier and integrator with over 50 years of experience designing, engineering, and installing turnkey systems tailored to each facility. From simple slider bed conveyors to complex multi-level incline systems, we deliver solutions built to perform from day one. Belt conveyors dominate the global conveyor market because of their versatility, speed (up to 600 FPM), and ability to handle a wide range of product types while integrating seamlessly with modern automation systems like WMS software, scanners, and robotics.
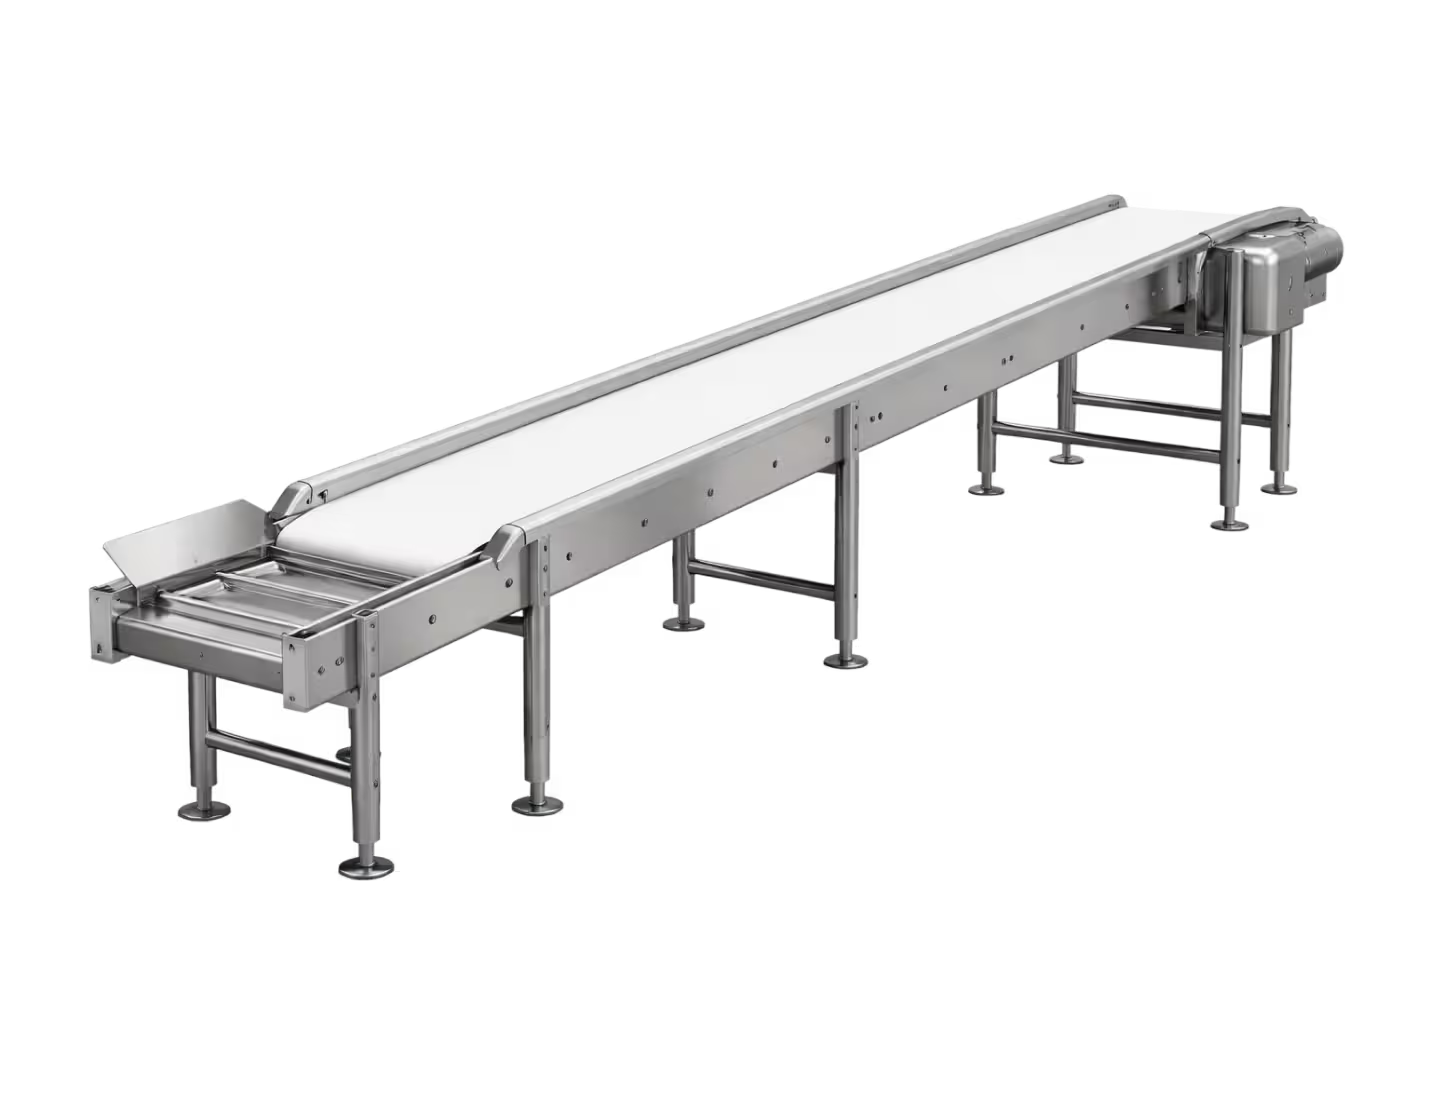
Driven by e-commerce and automation growth, the belt conveyor market is expected to exceed $5.5 billion by 2027, making it a key investment for long-term operational efficiency and competitiveness.
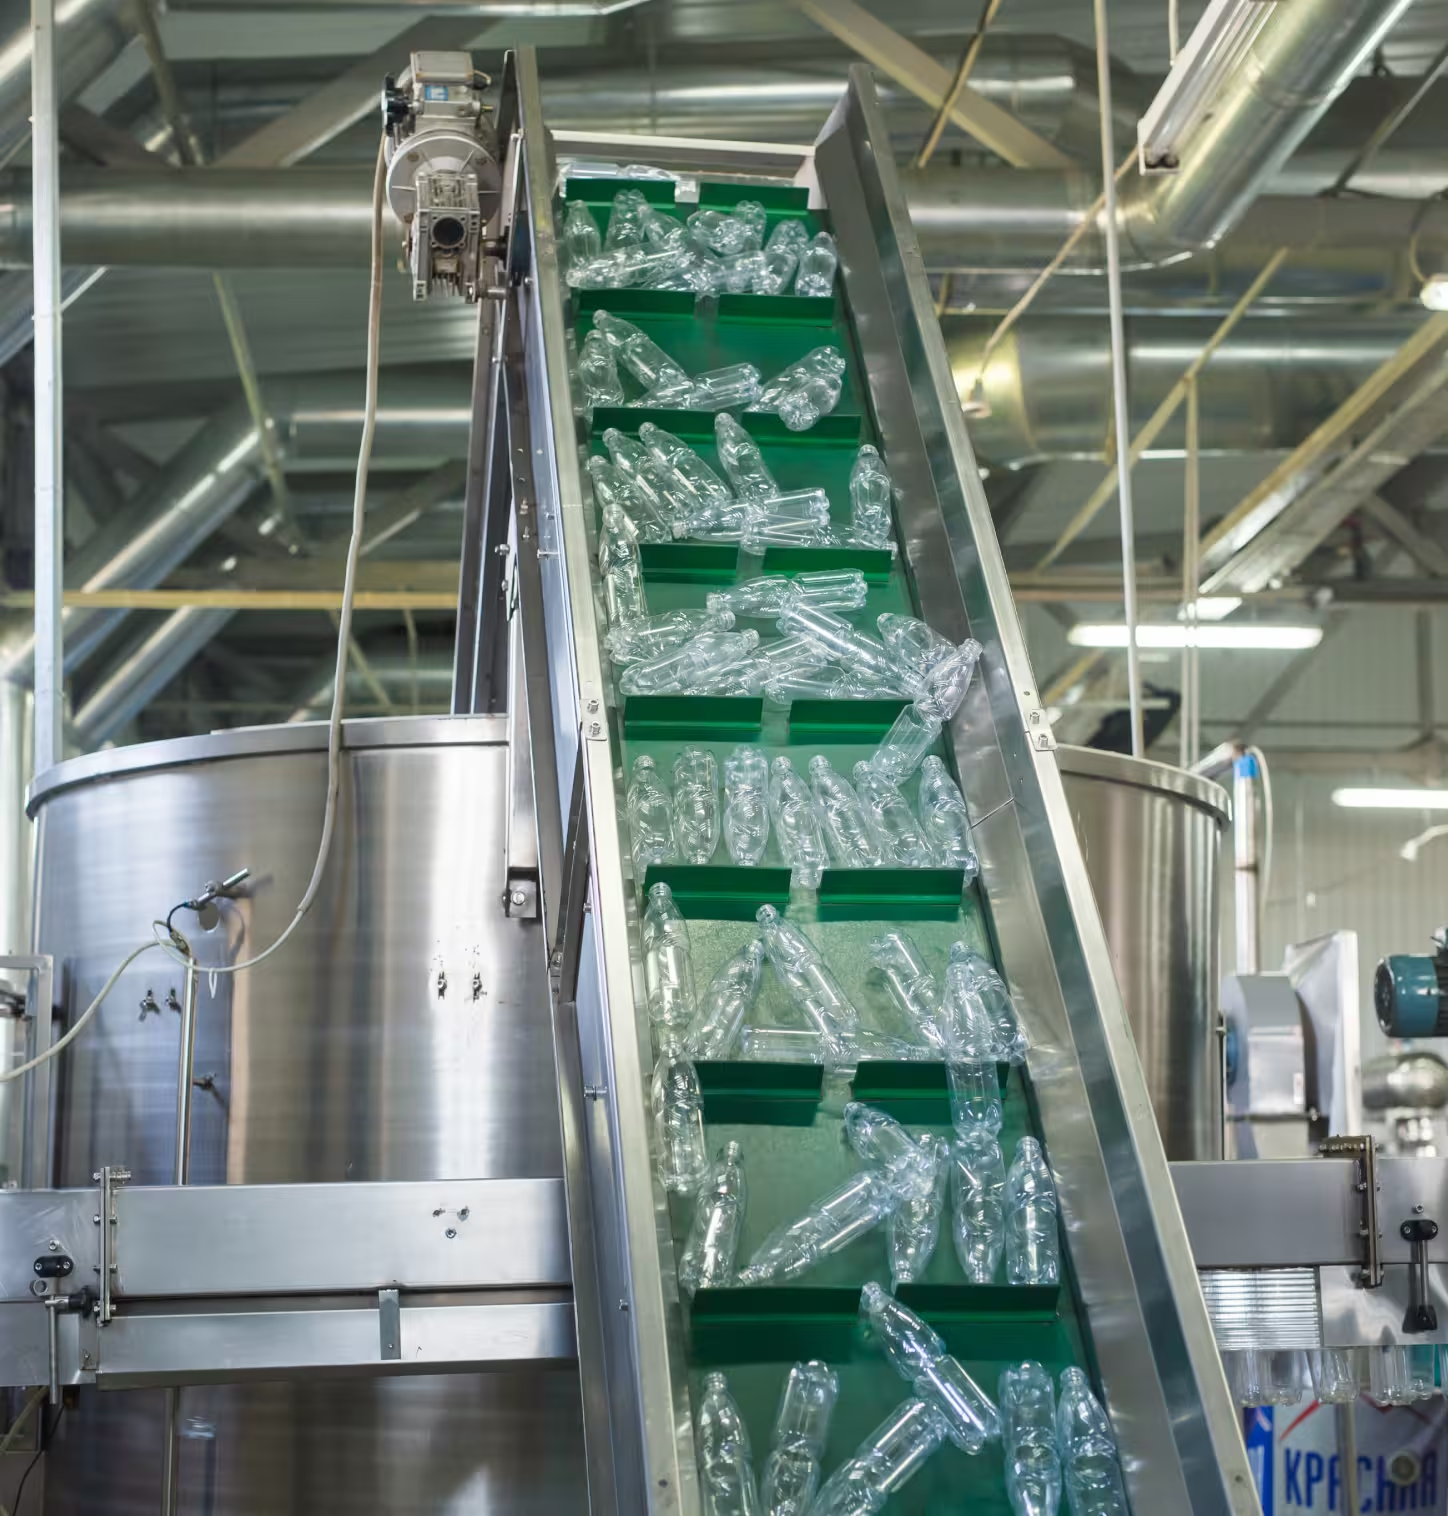
Types of Belt Conveyor Systems
We Supply & Install
Not all belt conveyors are the same. Different applications require different belt types, bed styles, and configurations. As an experienced belt conveyor integrator, MWS helps you select, configure, and install the exact belt conveyor system for your operation.
01
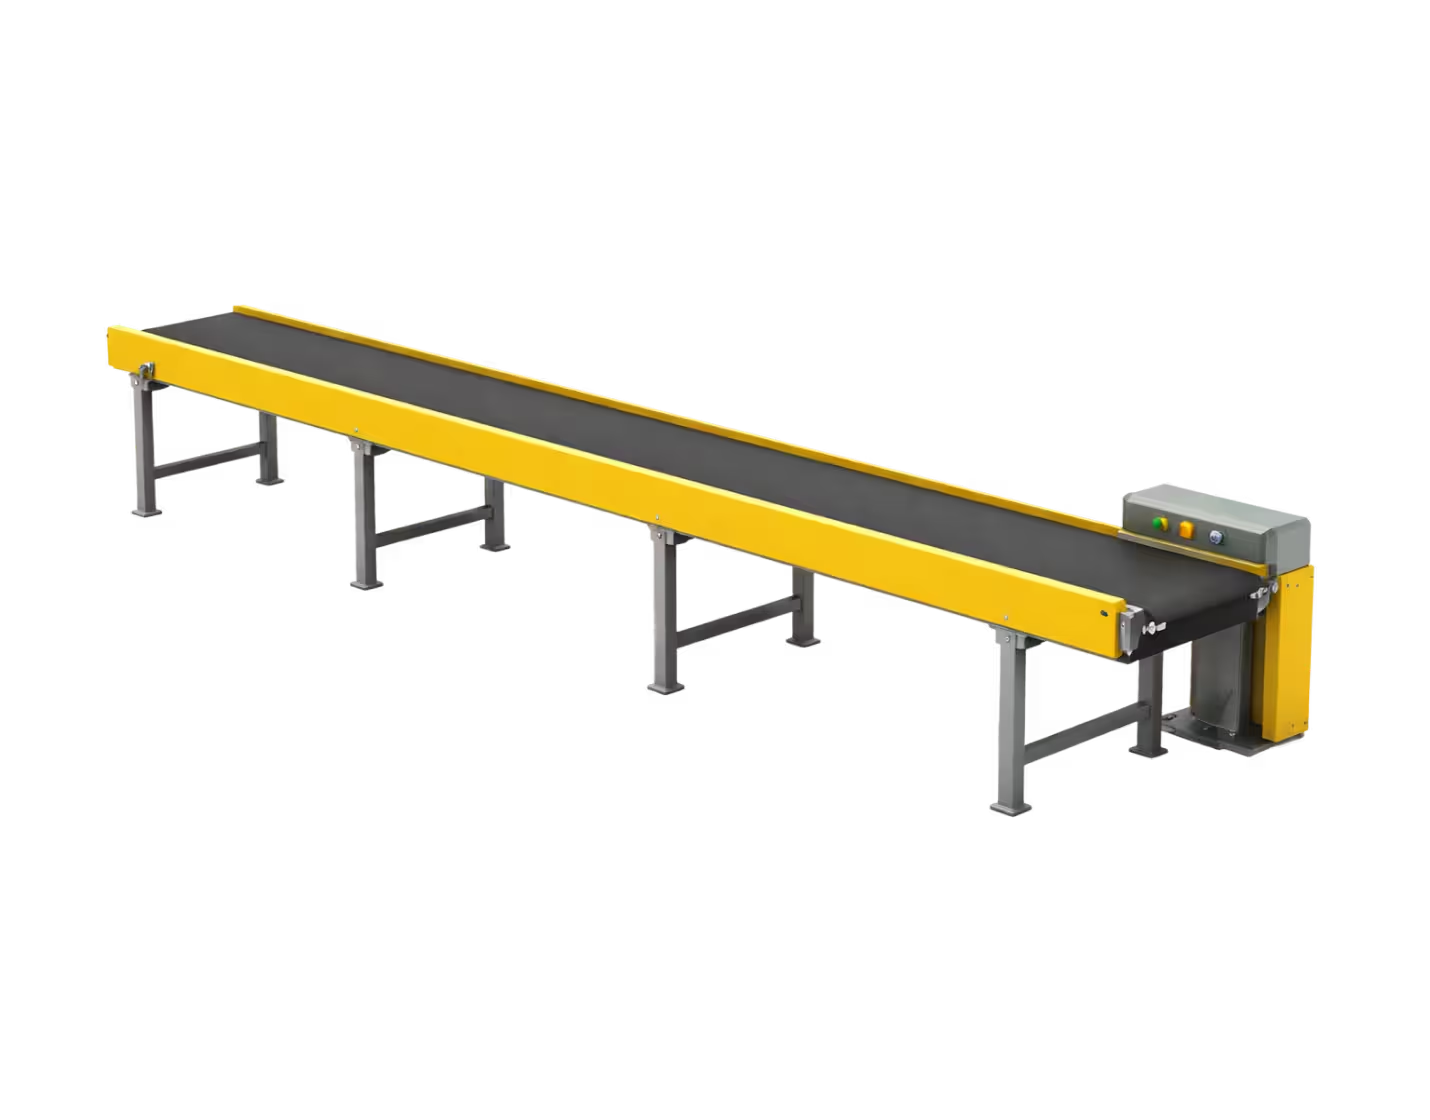
Slider Bed Belt Conveyors
Slider bed belt conveyors are the most common and economical type of belt conveyor system. The belt slides over a smooth steel or UHMW plate, providing a continuous, stable surface for product transport.
- Belt widths: 6" to 60"+
- Up to 300 FPM
- Up to 150 lbs/ft
- E-Commerce
- Distribution
02
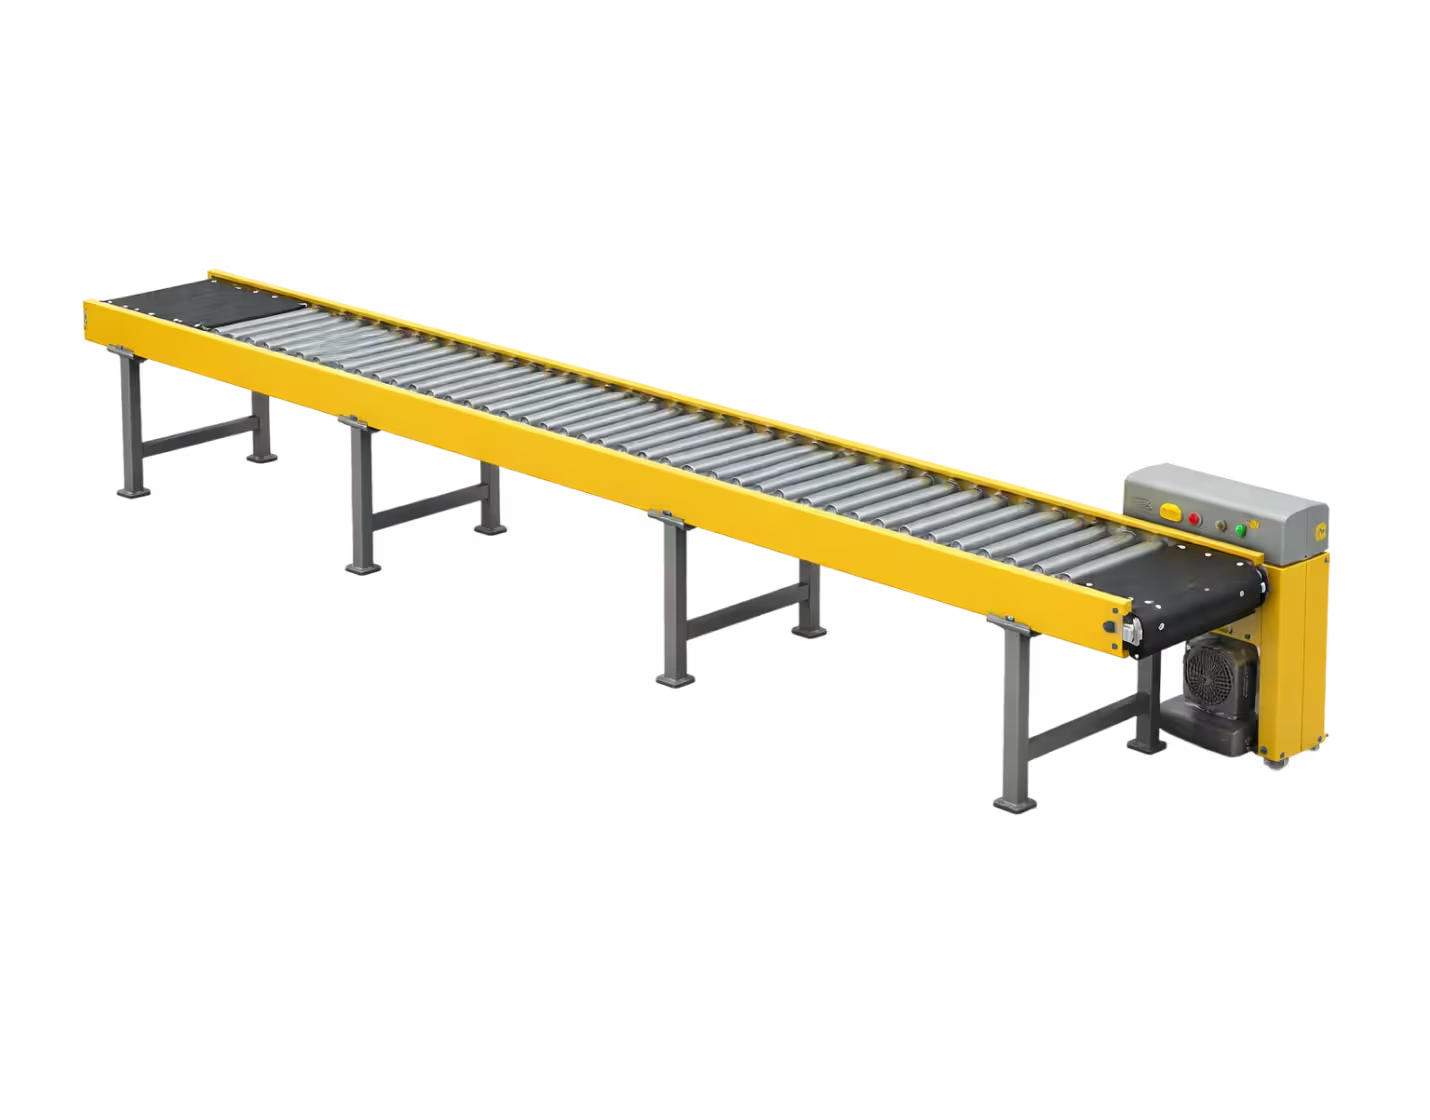
Roller Bed Belt Conveyors
Roller bed belt conveyors feature a series of rollers beneath the belt instead of a flat plate. The rollers reduce friction, allowing the system to handle heavier loads over longer distances with less motor power.
- Belt widths: 12" to 72"+
- Up to 600 FPM
- Up to 300+ lbs/ft
- Distribution
- Manufacturing
03
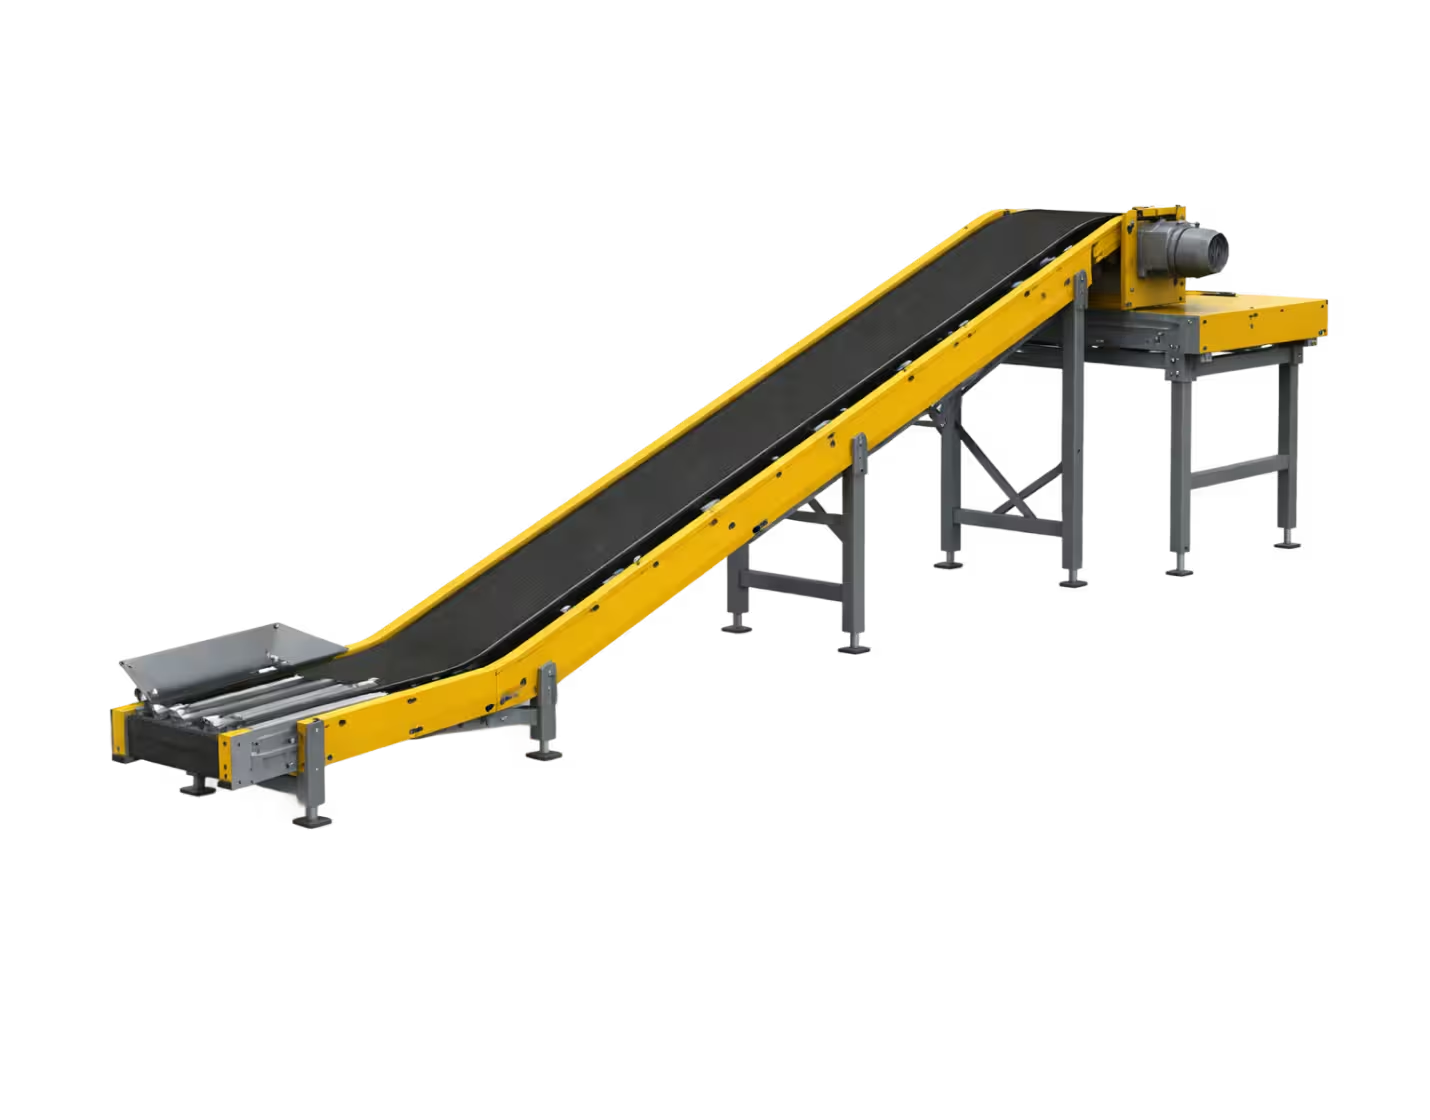
Incline & Decline Belt Conveyors
Incline belt conveyors and decline belt conveyors move products between different elevations — connecting ground floors to mezzanines, pick modules to packing areas, or receiving docks to storage levels.
- 5° to 30°+ incline
- Up to 300 FPM
- Multi-Level Warehouses
- E-Commerce
04
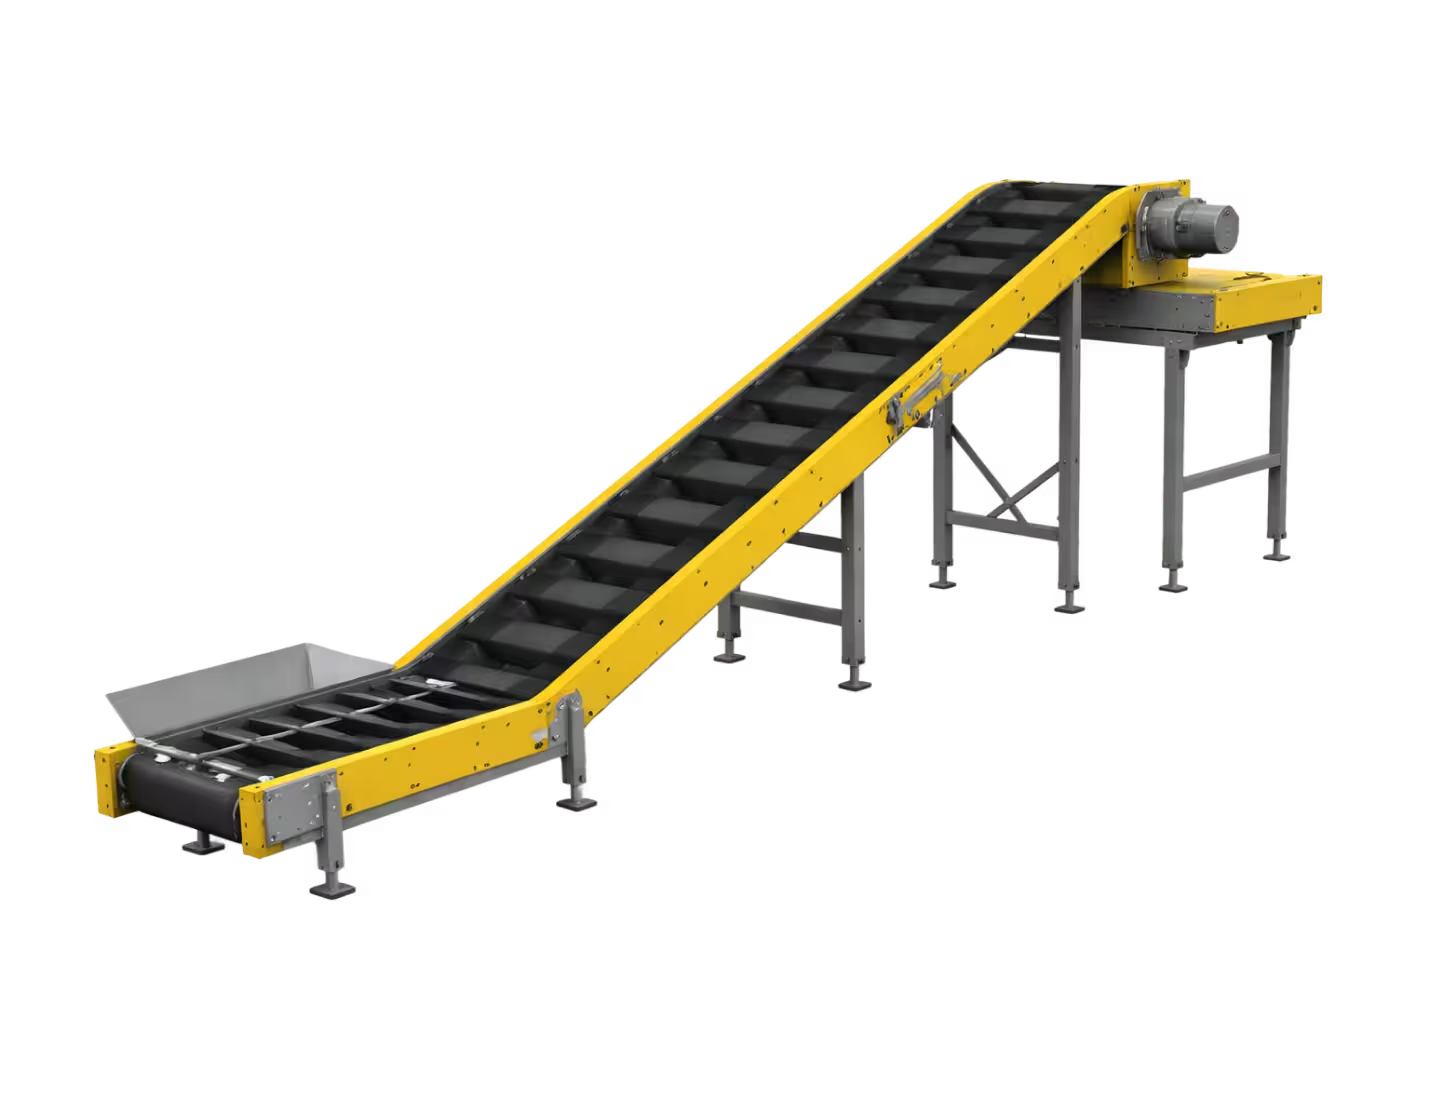
Cleated Belt Conveyors
Cleated belt conveyors feature vertical barriers (cleats) attached to the belt surface at regular intervals. These cleats prevent products from sliding backward on steep inclines or declines.
- Up to 45°+ incline
- Up to 200 FPM
- Manufacturing
- Food Recycling
05
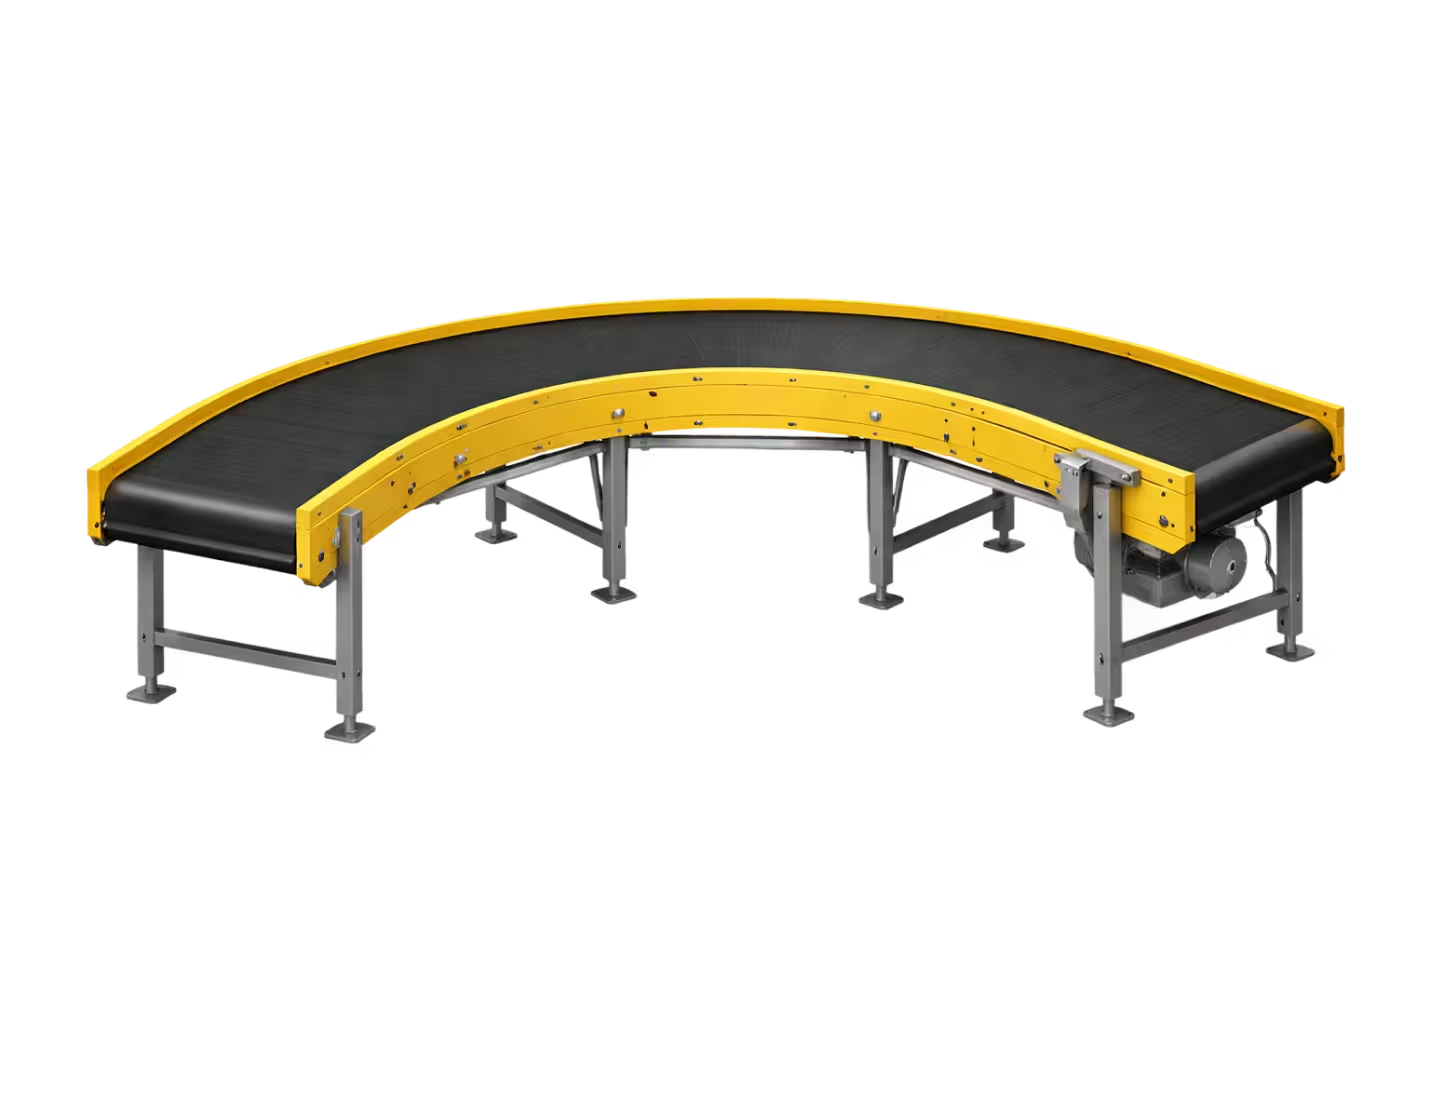
Curved Belt Conveyors
Curved belt conveyors change the direction of product flow — routing items around corners, through turns, and along winding paths without requiring a transfer point.
- 30°, 45°, 60°, 90°, 180° curves
- Up to 600 FPM
- E-Commerce
- Distribution
- Airports
06
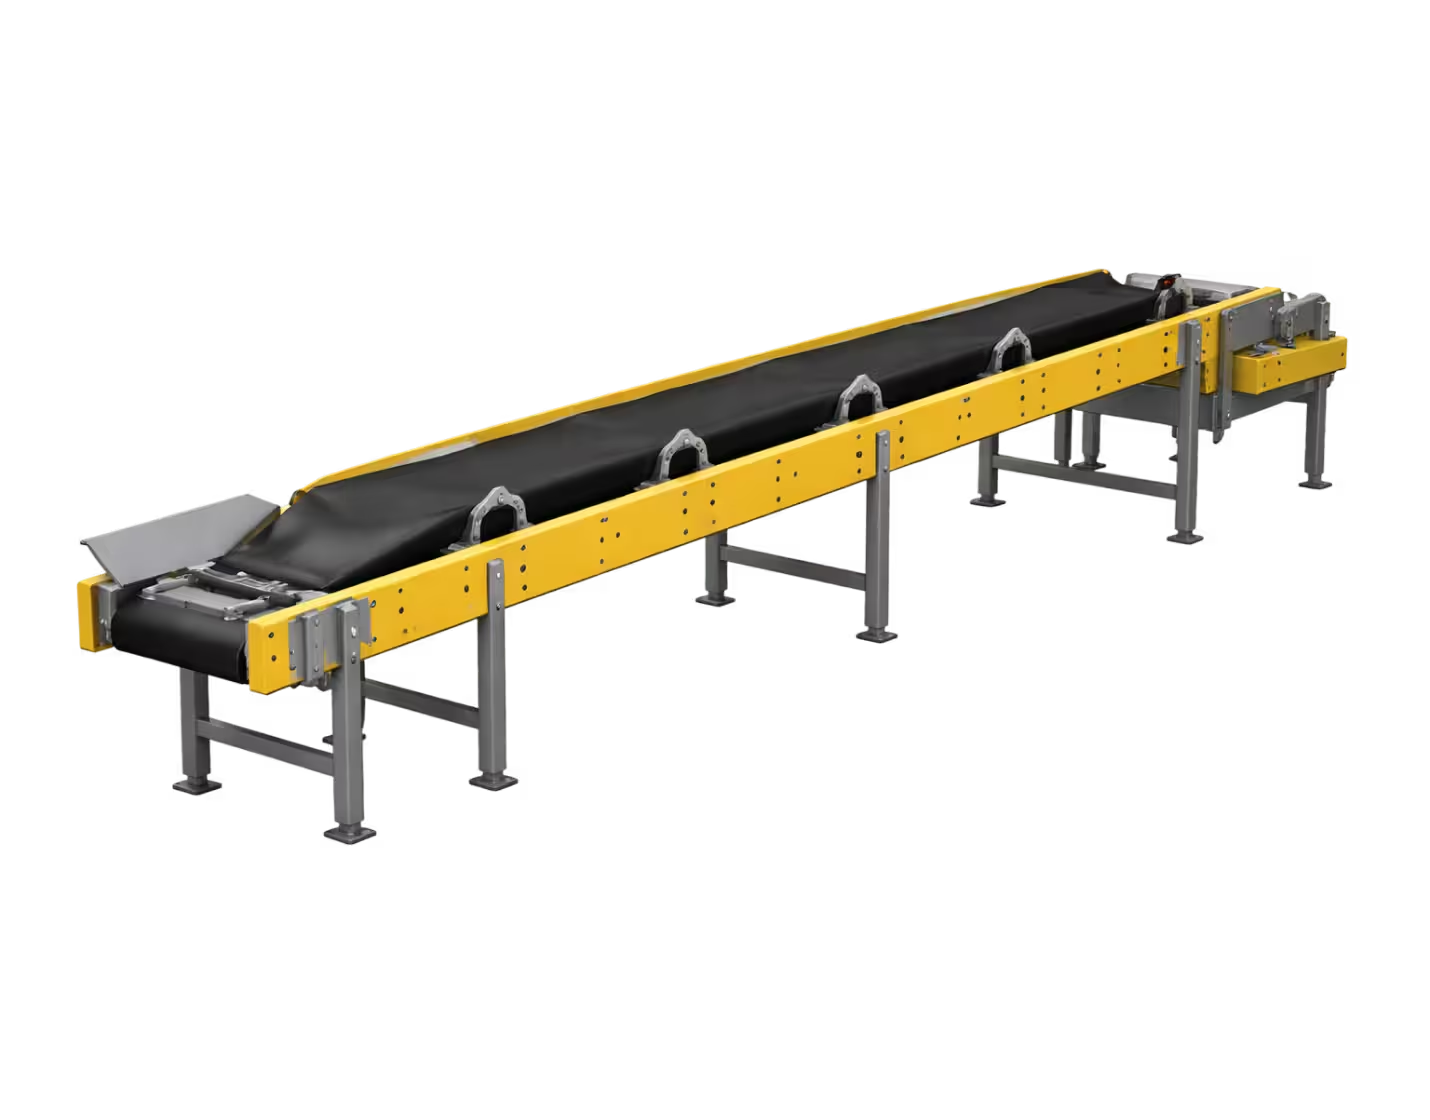
Troughed Belt Conveyors
Troughed belt conveyors shape the belt into a U-shaped channel using angled idler rollers. This trough design contains bulk materials — preventing spillage and increasing carrying capacity.
- Trough angles: 20°, 35°, 45°
- Belt widths: 18" to 96"+
- Recycling
- Mining
- Manufacturing
07
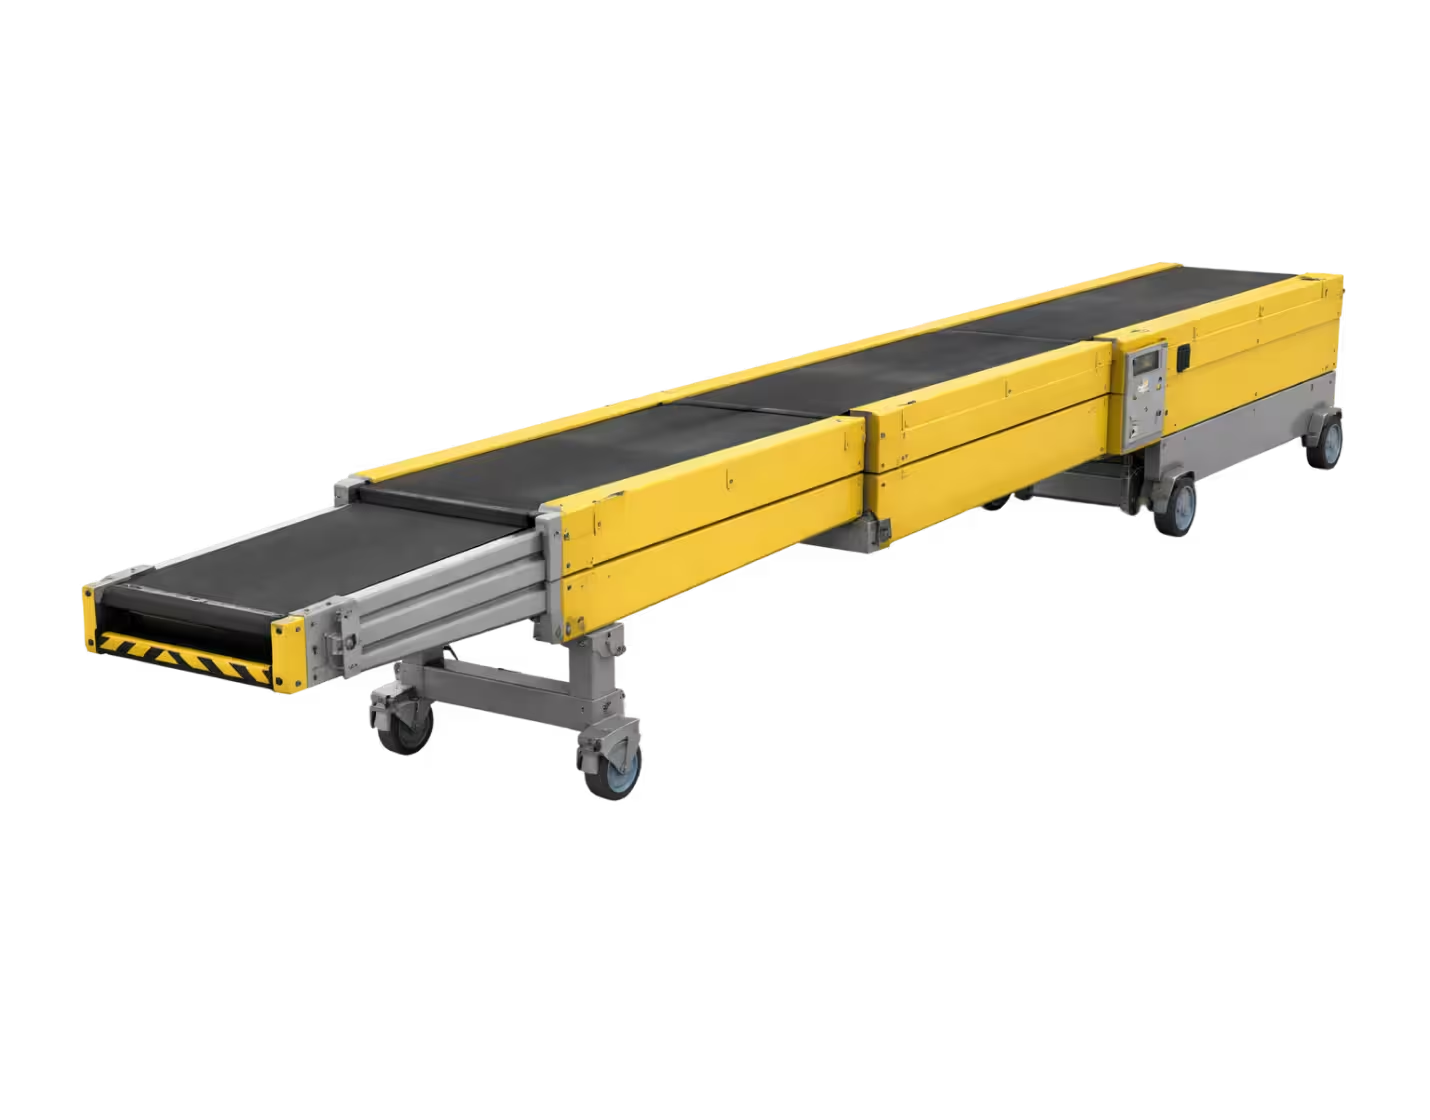
Telescoping / Extendable Belt Conveyors
Telescoping belt conveyors extend and retract to reach into truck trailers and shipping containers for loading and unloading, dramatically increasing loading/unloading speed.
- Up to 60+ feet extended
- Up to 75 lbs/pkg
- Distribution
- 3PL
- Retail
08
Sanitary / Washdown Belt Conveyors
Sanitary belt conveyors are designed for food processing, pharmaceutical, and cleanroom environments where hygiene, sanitation, and regulatory compliance are critical.
- Stainless steel (304/316)
- FDA/USDA approved
- IP65/IP69K rated
- Food & Beverage
- Pharmaceutical
Not Sure Which Belt Conveyor
Type Is Right for Your Operation?
Talk to a belt conveyor specialist who can evaluate your needs and recommend the best solution for your facility.
Or call us at 515-635-1555
Key Benefits of Belt
Conveyor Systems
Investing in belt conveyor systems delivers immediate and compounding returns across productivity, labor, accuracy, safety, and operational flexibility. Here's why belt conveyors are the most popular conveyor type in warehouse automation.
Unmatched Versatility
Belt conveyor systems handle the widest range of products of any conveyor type.
Product Protection
The smooth, continuous surface of a belt conveyor eliminates the gaps and transitions that can catch, tip, or damage products on roller conveyors.
High-Speed, Consistent Transport
Belt conveyors operate at speeds from 20 FPM (for precision applications) to 600+ FPM for high-throughput mainline transport.
Enhanced Order Accuracy
Integrate barcode scanners, RFID readers, and vision systems with your belt conveyor system for automated identification and routing.
Incline and Decline Capability
Need to move products between levels? Incline belt conveyors and decline belt conveyors transport items up and down slopes
Worker Safety
Belt conveyor systems eliminate the most common causes of warehouse injuries — manual lifting, carrying heavy loads
Reduced Labor Costs
Automate the repetitive, low-value task of moving products from point to point. Belt conveyor systems reduce material handling labor by 20–30%, allowing you to redeploy workers to higher-value tasks like picking, packing, quality control, and customer service.
Improved Throughput
Process 2–3x more orders per hour compared to manual material handling.
Space Flexibility
Belt conveyor systems run flat, climb inclines, descend declines, and navigate curves — all within the same continuous line. This geometric flexibility lets you route product flow through complex facility layouts, around obstacles, and between levels, maximizing every square foot of your warehouse.
Belt vs. Roller Conveyor Systems
The right conveyor depends on your products, facility layout, and workflow. Belt conveyors provide continuous support for small or irregular items, while roller conveyors work well for rigid, flat-bottomed cartons, totes, and pallets.
Compare the differences below to see where each fits your operation.
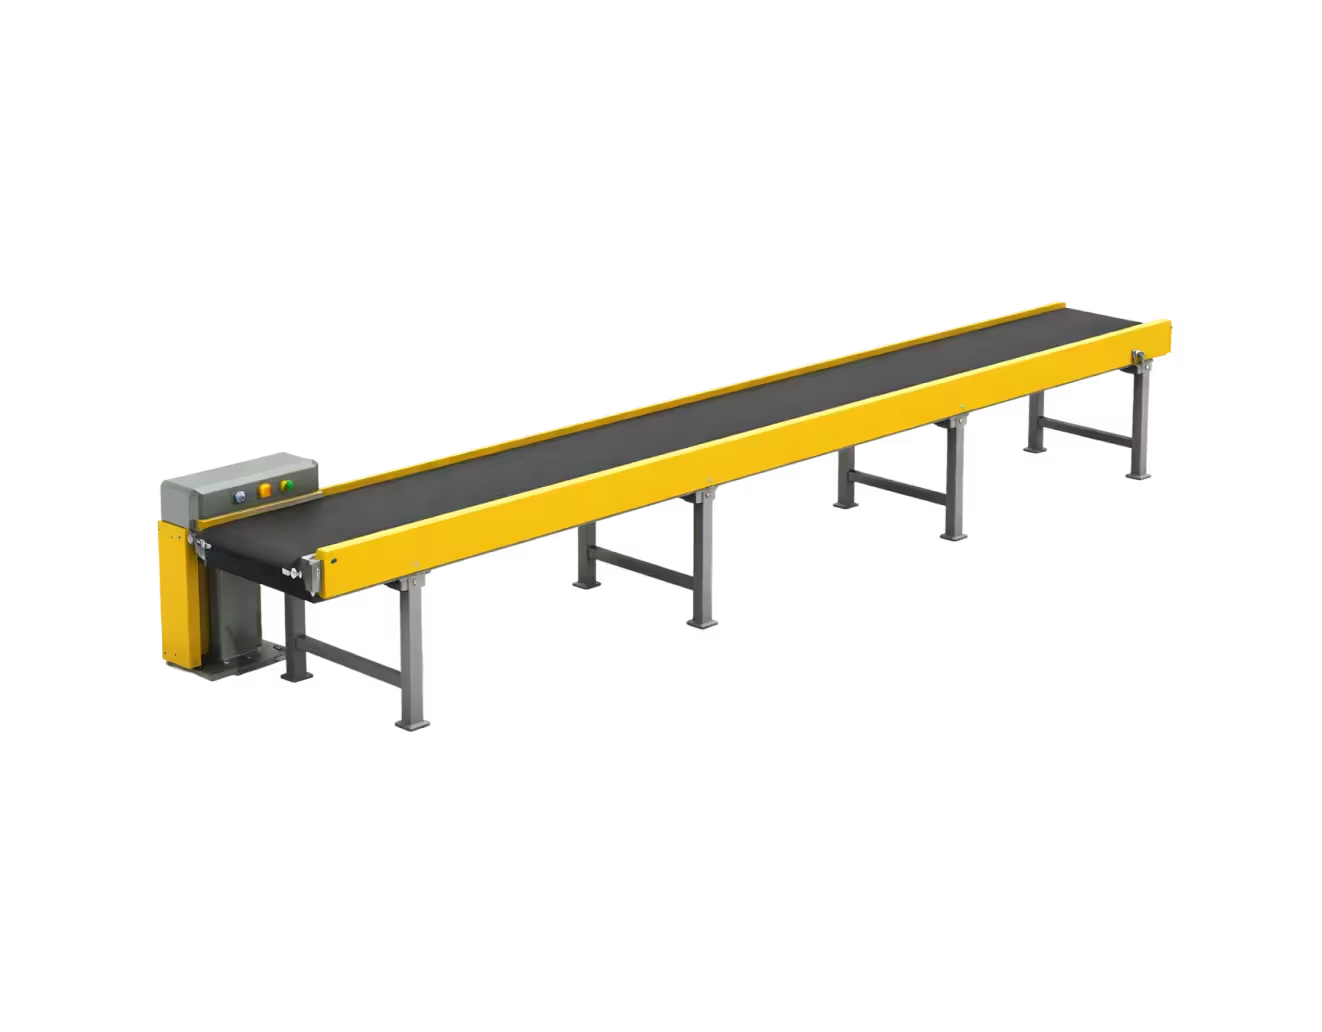
| Belt Conveyor Systems |
|---|
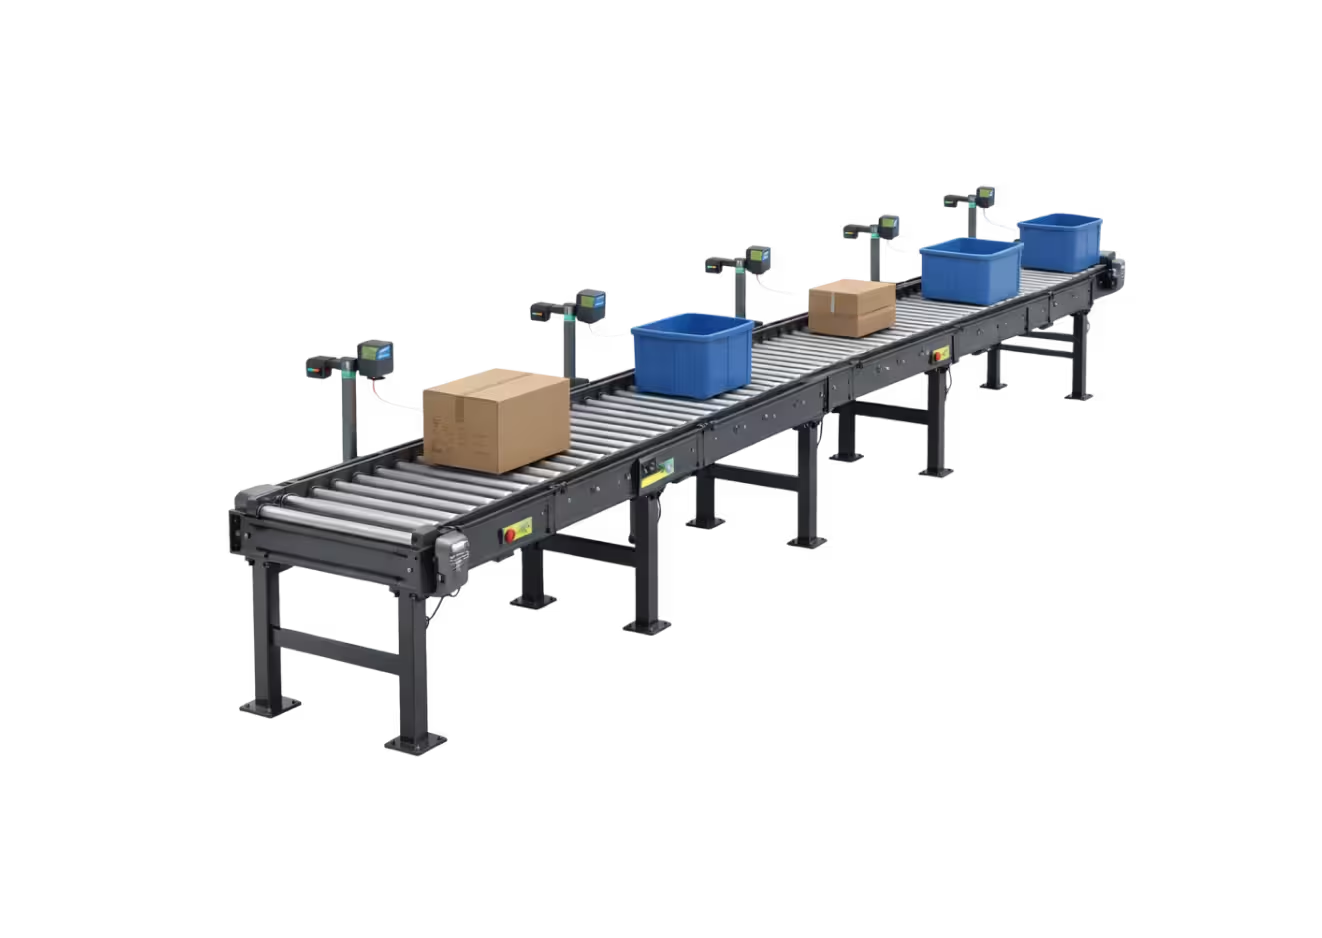
| Roller Conveyor Systems |
|---|
| Belt Conveyor Systems | Roller Conveyor Systems |
|---|---|
How to Choose the Right
Belt Conveyor System
Selecting the right belt conveyor system requires evaluating your products, throughput targets, facility layout, and automation needs. Here's a structured framework.
The best approach: Work with an experienced belt conveyor integrator like MWS. We evaluate all of these factors during our free, no-obligation consultation and recommend a belt conveyor system tailored to your exact needs.
Need Help Deciding Between Belt and Roller Conveyors?
Schedule a free consultation with our team. We'll evaluate your operation and recommend the best solution.
Or call us at 515-635-1555
Industries That Benefit from
Belt Conveyor Systems
Belt conveyor systems power operations across virtually every industry that moves products, packages, or materials at volume.
E-Commerce & Retail
- Belt Types: Slider bed, roller bed, incline, curved
- Applications: Order fulfillment, sortation feed, shipping
Polybags, envelopes, cartons, mixed SKUs
Manufacturing & Assembly
- Belt Types: Slider bed, roller bed, cleated
- Applications: Production line feeding, WIP transport, assembly
Parts, components, sub-assemblies
Parcel & Postal
- Belt Types: Slider bed, curved, incline
- Applications: Package sorting, scanning, shipping
Packages, parcels, flats, polybags
Food & Beverage
- Belt Types: Sanitary/washdown, incline, cleated
- Applications: Processing lines, packaging, ingredient transport
Packaged food, raw ingredients, bottles
Pharmaceutical & Healthcare
- Belt Types: Sanitary, slider bed, low-profile
- Applications: Cleanroom transport, order fulfillment, compliance
Medications, medical devices, lab supplies
Airports & Baggage Handling
- Belt Types: Curved, slider bed, incline
- Applications: Baggage transport, check-in, claim carousels
Luggage, oversized items
Distribution & 3PL
- Belt Types: Roller bed, slider bed, telescoping
- Applications: Mainline transport, cross-docking, dock loading
Cartons, totes, cases, parcels
Cold Storage & Frozen Goods
- Belt Types: Cold-rated belt, incline, roller bed
- Applications: Freezer-to-dock transport, cold chain logistics
Frozen food, cold-chain pharmaceuticals
Recycling & Waste
- Belt Types: Troughed, cleated, slider bed
- Applications: Sorting lines, material transport, scrap handling
Mixed recyclables, paper, plastics, metals
Why Choose MWS as Your
Belt Conveyor Systems Supplier
We don't just sell belt conveyor equipment — we design, engineer, install, and support complete belt conveyor systems. That's the integrator difference.
MWS vs. Other Belt Conveyor Suppliers — Comparison
| Capability | MWS (Full-Service Integrator) | Equipment-Only Dealer | Online Conveyor Retailer |
|---|---|---|---|
| Custom Belt Conveyor System Design | |||
| Multi-Brand Equipment Access | |||
| Belt Type & Configuration Expertise | |||
| Professional Installation | |||
| Controls & PLC Programming | |||
| WMS / ERP Integration | |||
| Commissioning & Training | |||
| Ongoing Maintenance & Support | |||
| Single Point of Accountability | |||
| 50+ Years of Warehouse Expertise |
Full-Service Belt Conveyor Integration
MWS manages every phase — from initial assessment and design to procurement, installation, PLC programming, WMS integration, and ongoing maintenance. One partner. One accountable team.
50+ Years of Warehouse Expertise
Founded in 1979, MWS brings over five decades of warehouse equipment and conveyor automation experience. We've designed and installed belt conveyor systems for operations of every size.
Top Manufacturer Partnerships
We partner with Hytrol, Dorner, Interroll, Dematic, and others — giving you access to premium belt conveyor equipment at competitive pricing.
Turnkey Automated Conveyor Solutions
From the first site visit to the final commissioning walkthrough and operator training — we handle your entire belt conveyor system project.
Midwest Service Coverage
Based in Iowa, serving belt conveyor installations across IA, IL, IN, MI, MN, MO, OH, WI, KS, NE, ND, and SD — with service teams that respond fast.
Single-Source Accountability
No finger-pointing between equipment vendors, electricians, and software providers. MWS is your single point of contact for your entire belt conveyor system project.
Our Proven Belt Conveyor System Installation Process
From initial assessment to ongoing support, our structured process ensures your belt conveyor system is designed right, installed right, and performs right — every time.
01
Consultation & Needs Assessment
Our team visits your facility to evaluate your current operations, product types, throughput requirements, elevation changes, and growth plans. We document every detail — no cost, no obligation.
WEEK 1-2
02
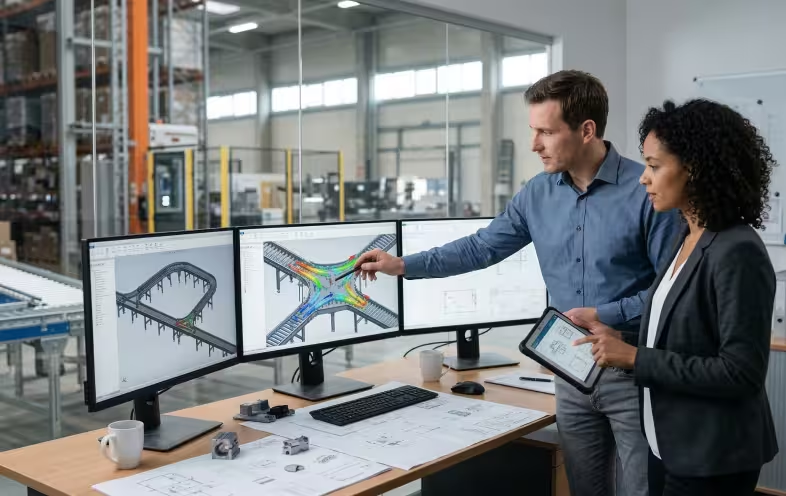
Custom Belt Conveyor
Design
Our engineers create a custom belt conveyor system layout using CAD modeling and simulation software. We select the optimal belt type, bed style, speed, width, and incline angles.
WEEK 3-6
03
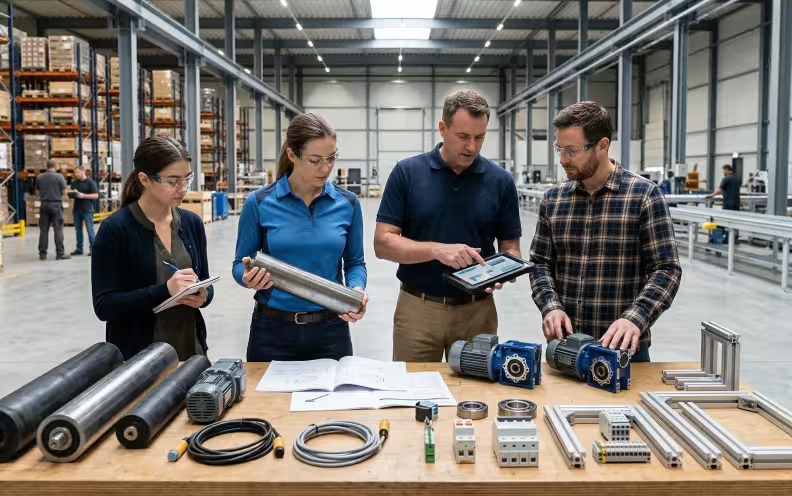
Equipment
Procurement
We source the best belt conveyor equipment from top manufacturers including Hytrol, Dorner, Interroll, Dematic. We leverage volume relationships for competitive pricing.
WEEK 6-12
04
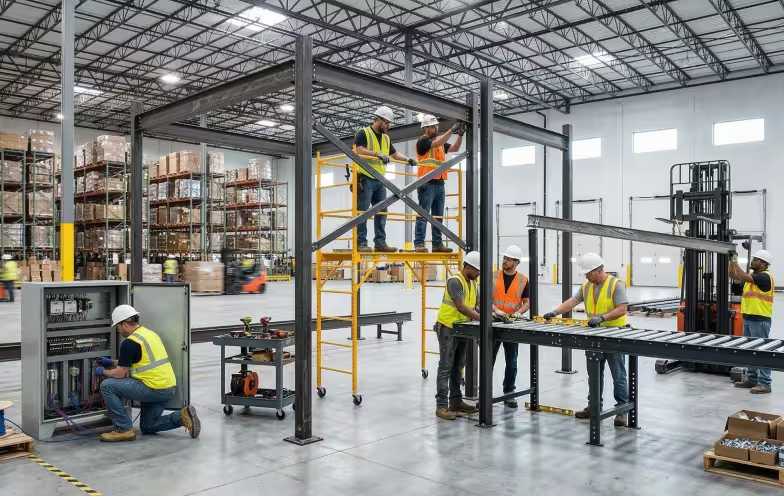
Professional
Installation
Our certified installation crews handle every aspect — structural steel, electrical, belt installation, controls wiring, and PLC programming. We minimize disruption to ongoing operations.
WEEK 12-24
05
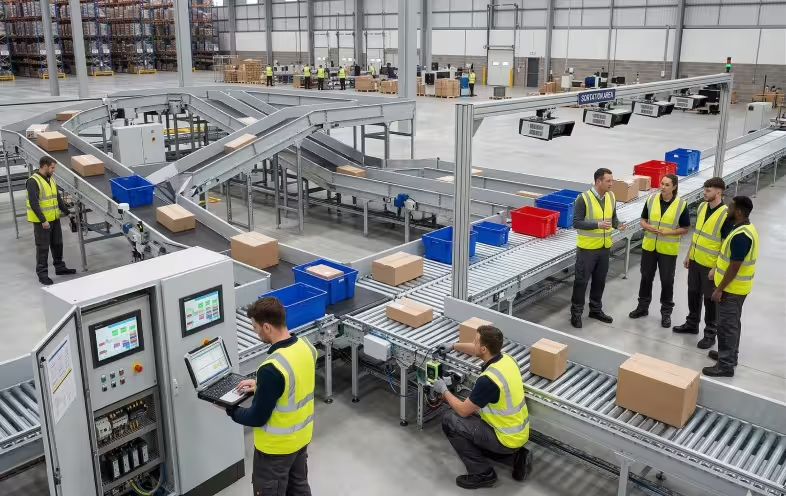
Testing, Commissioning
& Training
Every belt conveyor system undergoes rigorous testing. We run your actual products through every path, verify speeds, check tracking and tension, and train your operators.
WEEK 24-26
06
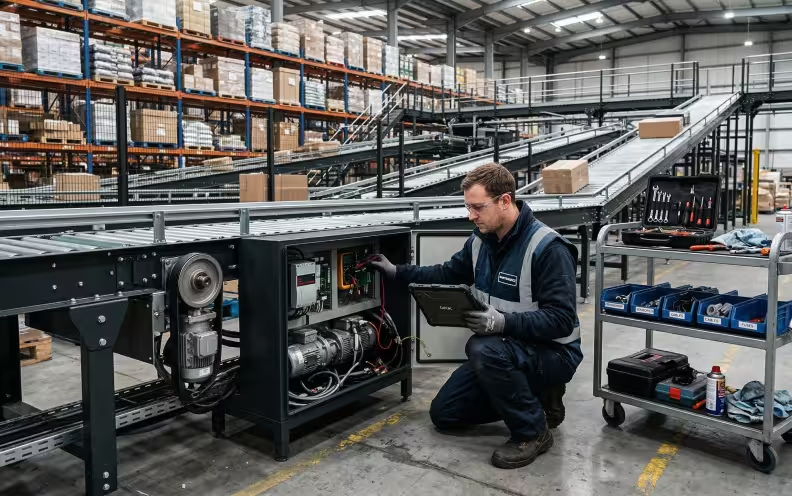
Ongoing Maintenance
& Support
We offer preventive maintenance programs, emergency service, belt replacement, spare parts, and system optimization reviews to keep your belt conveyors at peak performance.
ONGOING
Ready to Get Started?
Request a free consultation and let our team design a belt conveyor system built for your operation.
Or all us at 515-635-1555
Frequently Asked Questions About Belt Conveyor Systems
Get answers to the most common questions about belt conveyor systems, costs, installation timelines, maintenance, and specifications. These are the questions warehouse managers, operations directors, and facility planners ask most about belt conveyors.
How much do belt conveyor systems cost?
Belt conveyor system costs vary based on type, length, automation level, and installation complexity. As a general range: slider bed belt conveyors cost $150–$500 per linear foot; roller bed belt conveyors range from $300–$800 per linear foot; incline belt conveyors run $400–$1,000 per linear foot; and curved belt conveyors cost $800–$2,000 per linear foot. A simple slider bed belt conveyor line for packing or inspection may start under $15,000, while a complete belt conveyor system for a mid-sized warehouse typically ranges from $50,000 to $500,000+ depending on scope and complexity. The best approach is to contact a belt conveyor systems supplier like MWS for a free consultation and custom quote. Call 515-635-1555 for a no-obligation estimate.
What is the difference between a slider bed and roller bed belt conveyor?
A slider bed belt conveyor has the belt sliding over a smooth flat plate (steel or UHMW plastic), while a roller bed belt conveyor has a series of rollers beneath the belt. The key differences: Slider bed — lower cost, ideal for light to medium loads (up to ~150 lbs/ft), best for shorter runs, packing lines, and general-purpose transport. Slightly higher friction means more motor power needed for long runs. Roller bed — rollers reduce friction dramatically, enabling heavier loads (up to 300+ lbs/ft), longer distances, and higher speeds with less motor power. Costs more upfront but handles heavy-duty applications that slider beds cannot. Most MWS belt conveyor designs use slider bed for lighter, shorter sections and roller bed for heavy, long-distance mainlines.
What belt speeds are typical for warehouse belt conveyor systems?
Belt conveyor speeds in warehouse applications typically range from 20 FPM to 600+ FPM, depending on the application. Operator loading zones run at 20–65 FPM for safety. Packing and inspection lines operate at 40–100 FPM. Scanning and weighing stations use 80–200 FPM for accurate reads. General mainline transport runs at 200–400 FPM. High-speed sortation feeds reach 400–600+ FPM. Variable frequency drives (VFDs) allow belt conveyor systems to adjust speed automatically based on zone requirements, accumulation needs, and downstream readiness — providing a continuous, optimized flow throughout your facility.
Can belt conveyor systems integrate with WMS and automation equipment?
Yes. Modern belt conveyor systems integrate seamlessly with all major warehouse management systems (WMS), including SAP, Oracle WMS, Manhattan Associates, Blue Yonder, Körber, HighJump, and many others. Integration is achieved through PLCs that communicate via standard protocols (OPC-UA, APIs, middleware) with your WMS to receive routing instructions, update inventory, and coordinate with other automation systems. Belt conveyors also integrate with barcode scanners, RFID readers, print-and-apply labelers, robotic picking arms, automated storage and retrieval systems (AS/RS), and sortation equipment. MWS handles all WMS and automation integration as part of our turnkey belt conveyor system installation.
Can belt conveyor systems work in cold storage and freezer environments?
Yes. Specialized belt conveyor systems are available for cold storage and freezer environments operating at temperatures as low as -20°F to -40°F. These systems use cold-rated components including: cold-temperature belt material (PVC and PU compounds rated for sub-zero operation); stainless steel or cold-rated steel frames; low-temperature lubricants for bearings and moving parts; sealed motors rated for freezer operation; and moisture-resistant electrical components. Cold storage belt conveyor systems reduce worker exposure to hazardous freezer environments, maintain product integrity through the cold chain, and improve throughput in temperature-sensitive supply chains. MWS designs and installs cold storage belt conveyor systems for food, pharmaceutical, and frozen goods operations across the Midwest.
Plan Your Project
with Our Team
Free consultation
Request a Free Belt
Conveyor System Quote
Tell us about your operation and our team will design a custom belt conveyor system tailored to your requirements. No obligation. Fast response. 50+ years of expertise behind every recommendation.
Or all us at 515-635-1555
Save time. We will contact you
Provide your details, and we’ll help you find exactly what you need