
AUTOMATED CONVEYORS
Automated Conveyor Systems from a Top Warehouse Conveyor Supplier & Integrator
We design, supply, and install automated conveyor systems that move your warehouse operations forward — increasing throughput, reducing labor costs, and maximizing every square foot of your facility.
Speak with an expert  515-635-1555
Home / Warehouse Equipment / Conveyors and Automated Systems / Automated Conveyors
Conveyor Systems Designed Around Your Operation
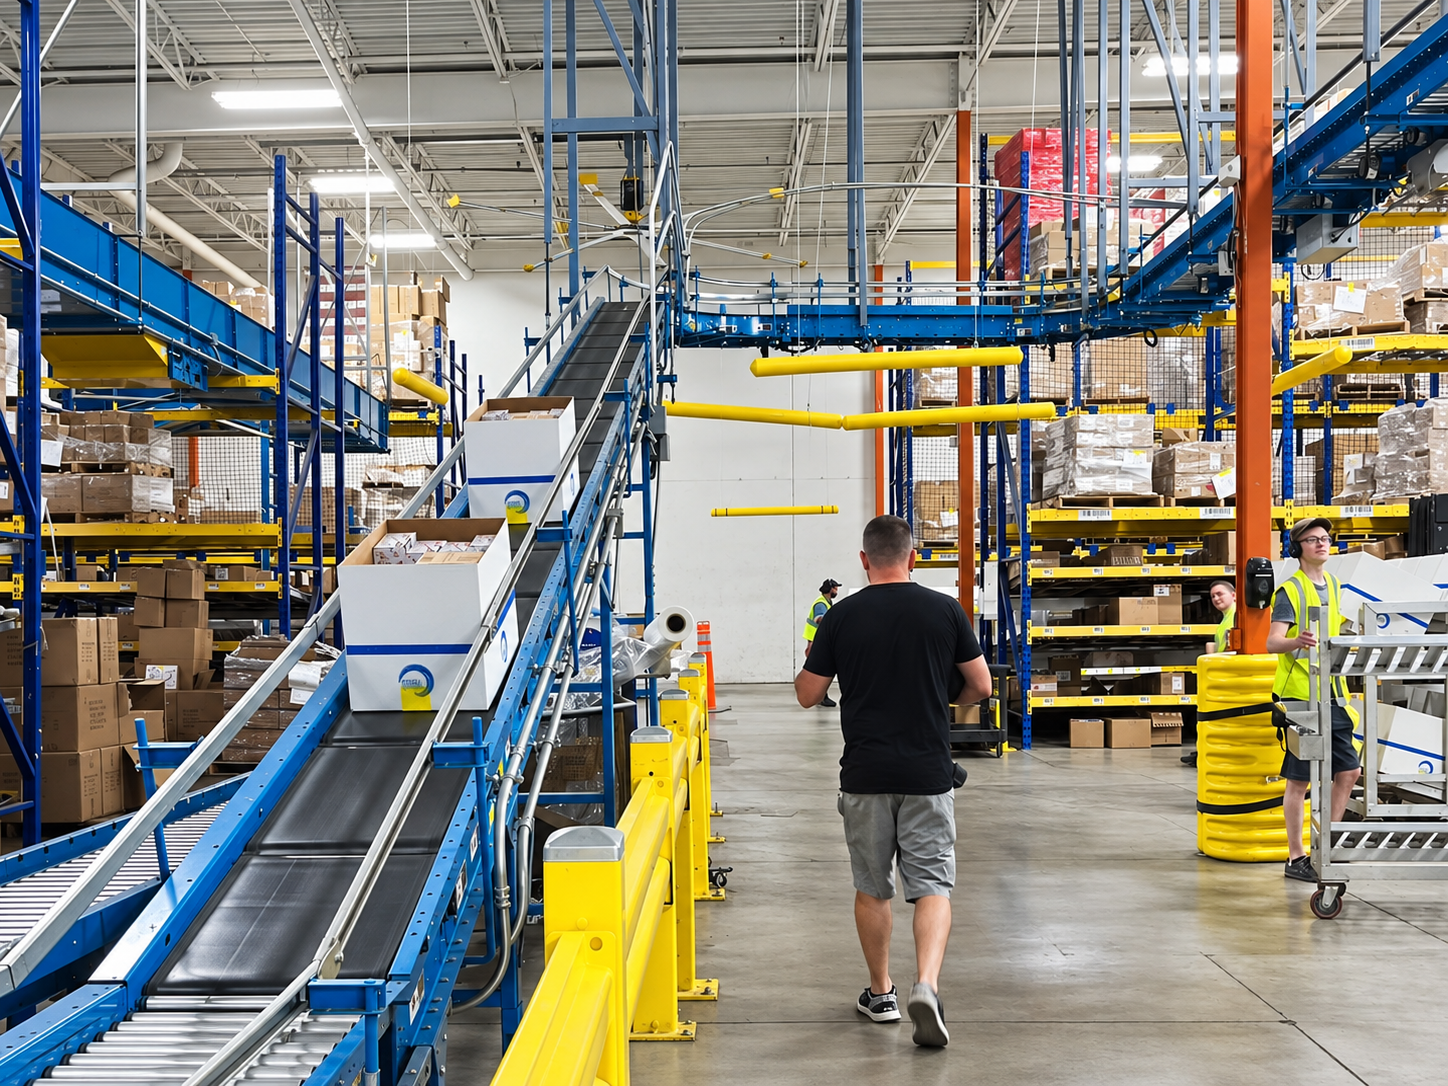
MWS plans, designs, and installs conveyor solutions ranging from simple product transfers to fully automated fulfillment systems. We work with your team to assess how products move through your operation, from picking and packing to labeling and truck loading, and identify the equipment and level of automation that best fit your workflow.
By reviewing current throughput, capacity requirements, and growth plans, we develop a layout that meets today’s needs and supports future expansion. Whether you need a basic conveyor line or an integrated system, MWS helps you plan improvements and add automation as your operation grows.
For all Conveyor System Projects
Turn-Key Design, Sales, Installation
& Preventative Maintenance
01
Planning & Design
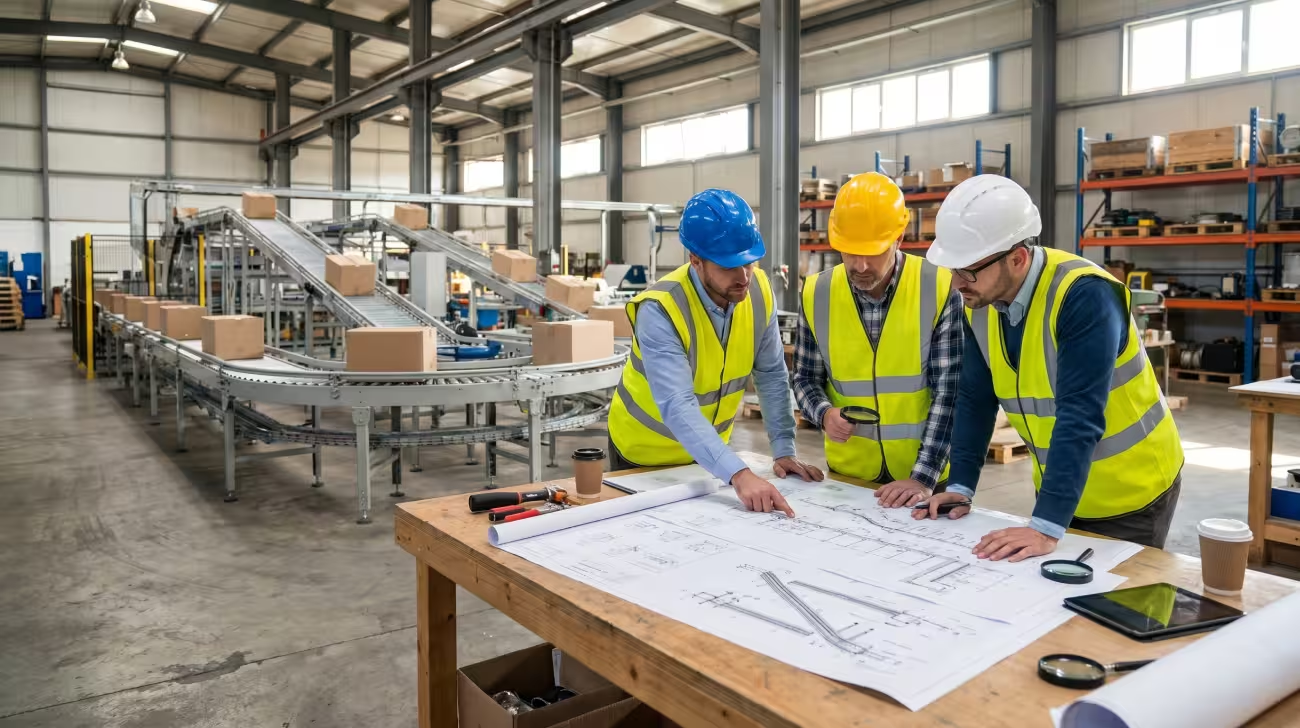
MWS offers comprehensive automated conveyor system design and consultation for projects of any size — from a single conveyor line to full-facility material handling layouts. Our team of experienced conveyor engineers and equipment-to-controls specialists evaluate your throughput, product mix, and floor plan to design a system that fits your operation exactly.
- Full facility assessment and conveyor layout design
- CAD modeling and 3D conveyor system simulation
- Integration with existing warehouse management systems (WMS)
- Scalable designs that grow with your throughput
02
Installation
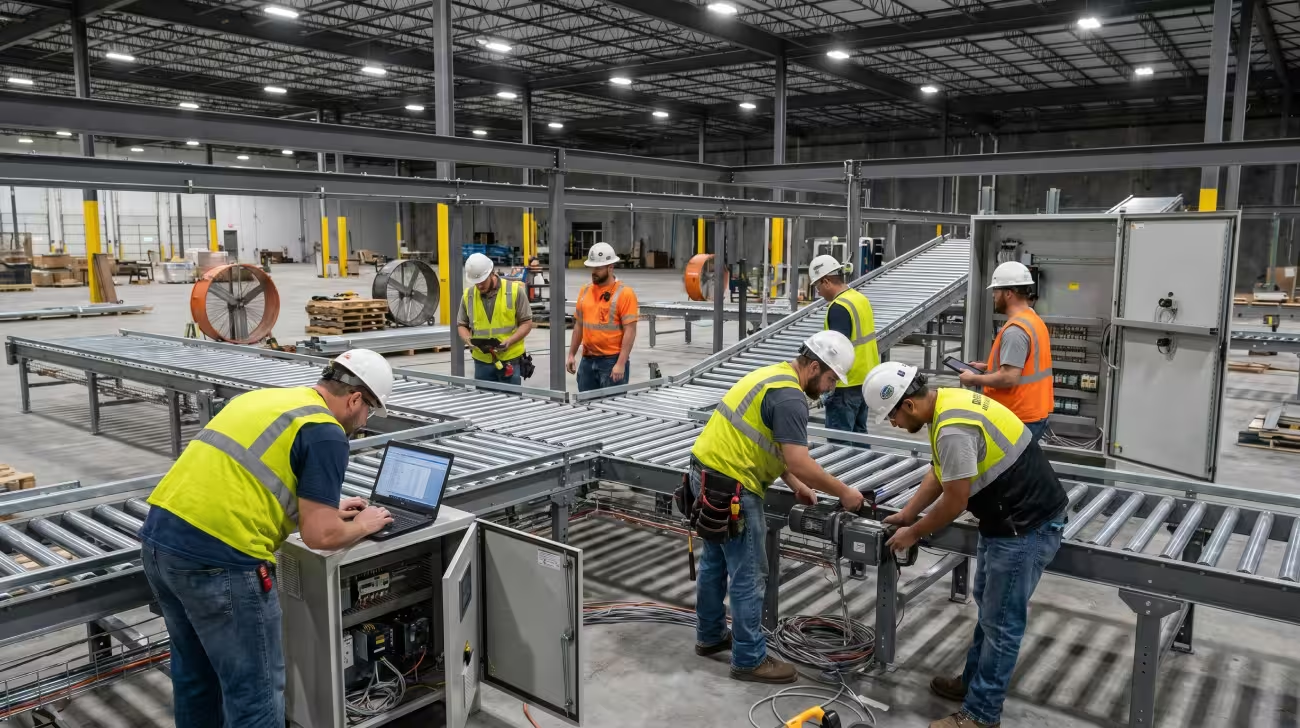
Our certified installation crews handle every phase of your automated conveyor system build-out — structural steel, electrical, controls, software, and testing. MWS minimizes disruption to your ongoing warehouse operations with carefully phased installation plans, and our team stays on-site until every conveyor line is running at full specification.
- Certified conveyor installation technicians
- Electrical, controls, and PLC programming in-house
- Phased installation to minimize operational downtime
- Full commissioning, testing, and staff training included
03
Ongoing Support
Preventative maintenance long after start-up is complete is just the beginning of automated conveyor system ownership. It's imperative that experienced technicians regularly monitor and maintain chains, bearings, belt alignments, motors, sensors, and controls to prevent costly breakdowns. Having adequate spare parts inventory on hand is also critical to minimizing unplanned downtime.
- Scheduled preventative maintenance programs
- Chain, bearing, belt, motor, and sensor maintenance
- Critical spare parts inventory management
- Emergency conveyor repair response across the Midwest
Types of Automated Conveyor
Systems We Supply & Install
Every warehouse is different. That's why MWS offers a complete range of automated conveyor system types — each designed for specific applications, product characteristics, and throughput requirements. As an experienced conveyor system integrator, we help you select, configure, and install the right system for your operation.
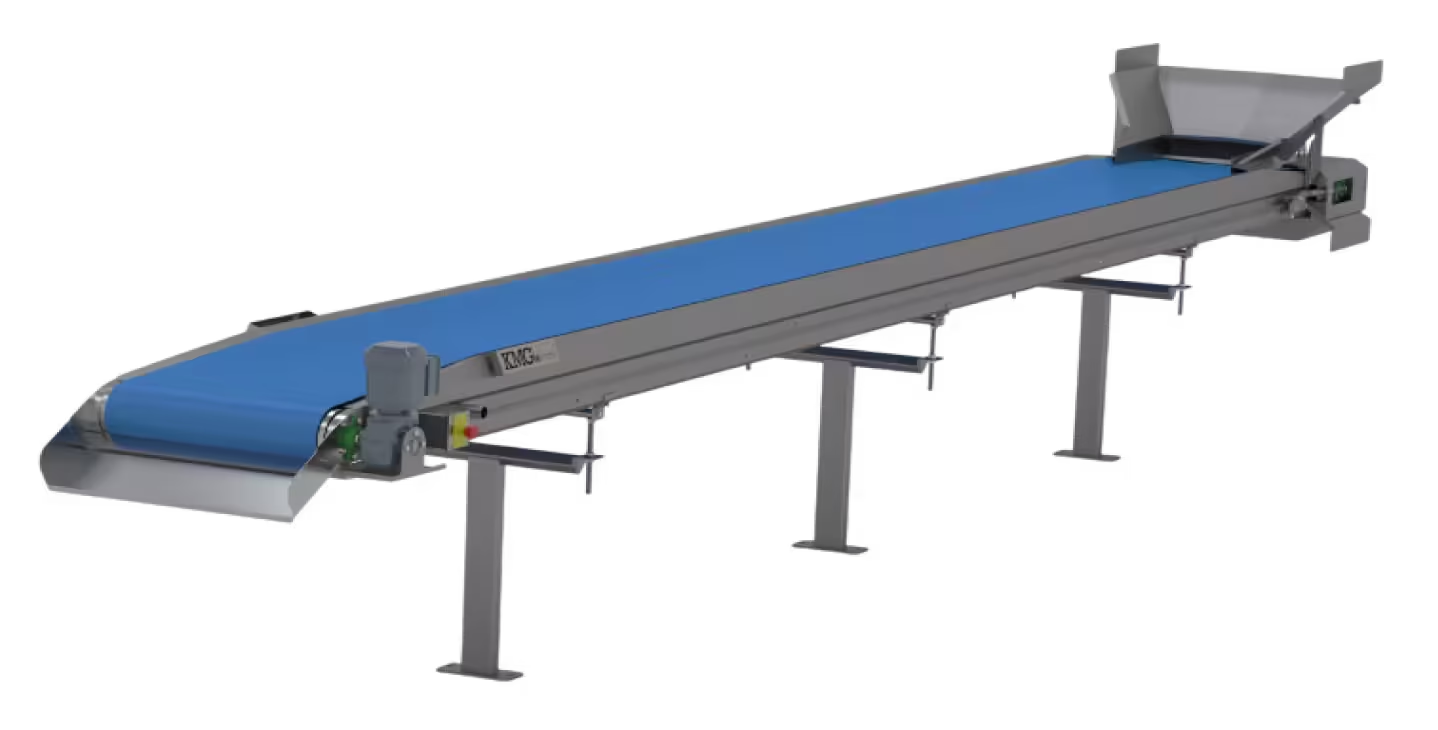
01
Belt Conveyor Systems
Belt conveyors are the workhorse of warehouse automation. They use a continuous belt stretched over pulleys to transport packages, individual items, and bulk materials along flat, inclined, or declined paths. Belt conveyors handle a wide variety of product sizes and weights, making them the most versatile automated conveyor system option for distribution centers and e-commerce fulfillment operations.
At MWS, we supply and install belt conveyor systems from leading manufacturers — configuring belt width, speed, incline angle, and accumulation features to match your specific throughput and product mix requirements.
- Best for: Packages, bulk materials, inclined transport
- Industries: E-Commerce, Distribution, Manufacturing
- Speed Range: Up to 600 FPM
02
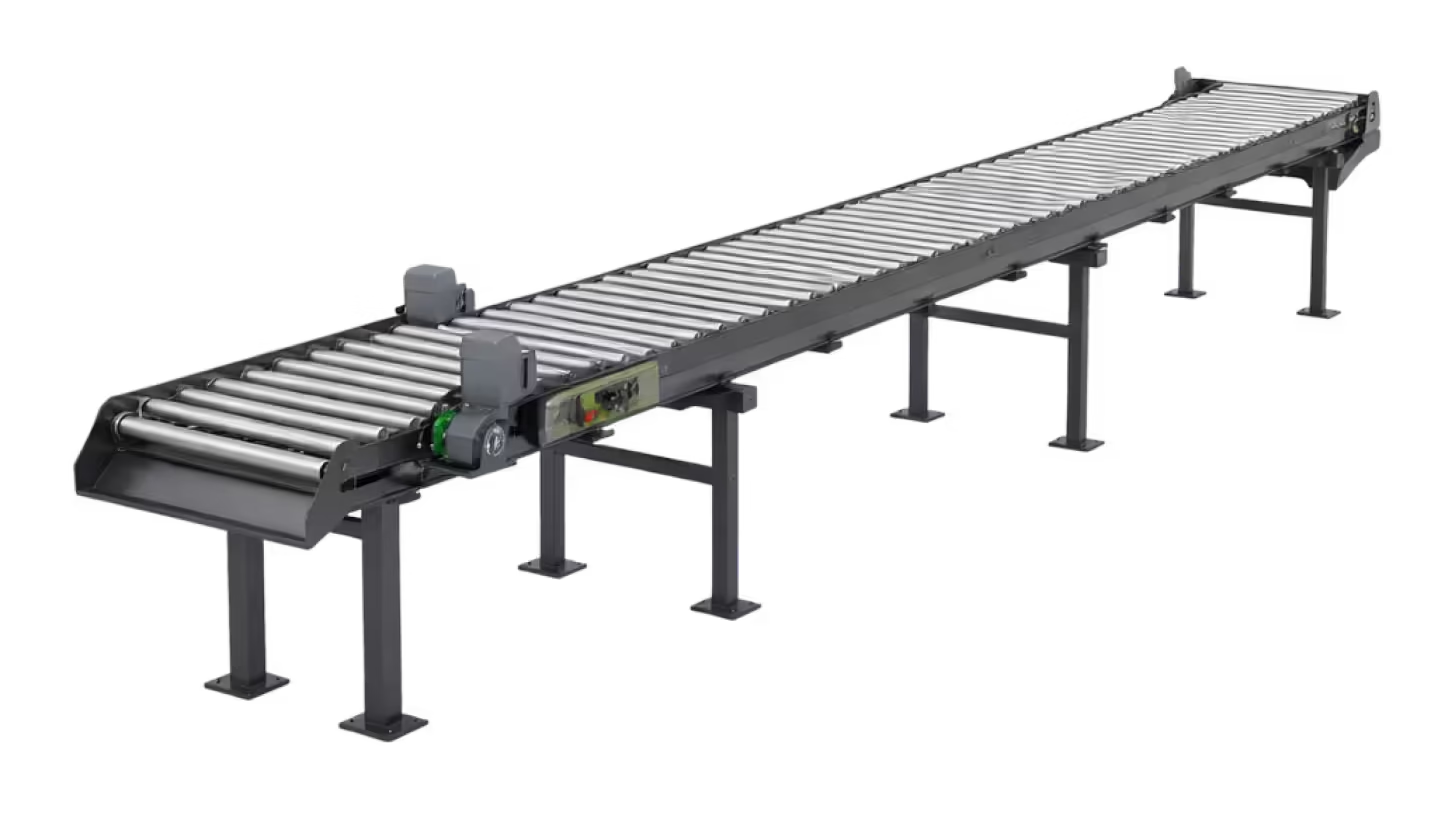
Roller Conveyor Systems (Powered and Gravity)
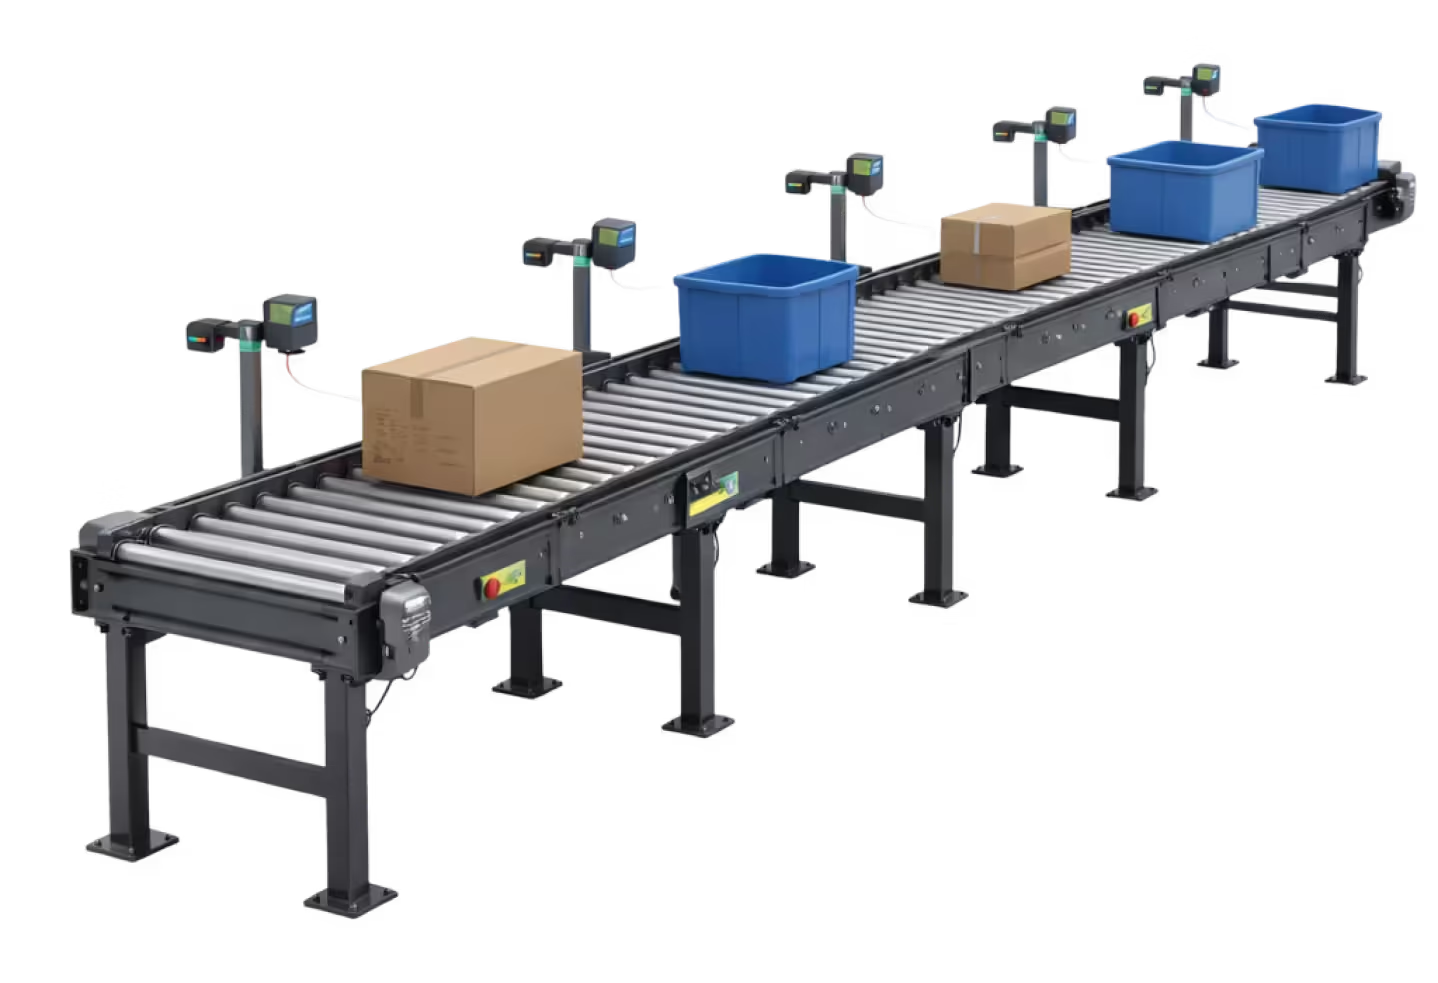
Powered roller conveyors use motor-driven rollers to move products at controlled, consistent speeds. They are ideal for transporting boxes, totes, cartons, and pallets with flat bottoms, and they support advanced features like zero-pressure accumulation — where products queue without touching or damaging each other.
Gravity roller conveyors are unpowered conveyor systems that use a slight decline or manual force to move products. They offer a cost-effective, low-maintenance solution for simple point-to-point transfers, staging areas, and workstation feeds.
Most modern warehouse conveyor systems combine both powered and gravity sections for optimal efficiency and cost-effectiveness.
- Best for: Boxes, totes, cartons, pallets
- Industries: Distribution, 3PL, Retail
- Speed Range: Up to 300 FPM (powered)
03
Accumulation Conveyor Systems
Accumulation conveyors act as intelligent buffers in your material handling conveyor system. They allow products to queue in a controlled manner — without back pressure, product contact, or damage — while downstream processes catch up. This is critical for balancing flow between operations that run at different speeds.
Zero-pressure accumulation conveyors use photo-eye sensors and individually controlled zones to stop products with gaps between them, protecting fragile items. Minimum-pressure accumulation systems allow light contact between products, suitable for durable goods. Both types keep your entire automated conveyor system running smoothly, even when one area slows down.
- Best for: Buffering, flow balancing, protecting fragile products
- Industries: Manufacturing, Distribution
- Speed Range: Up to 200 FPM
04
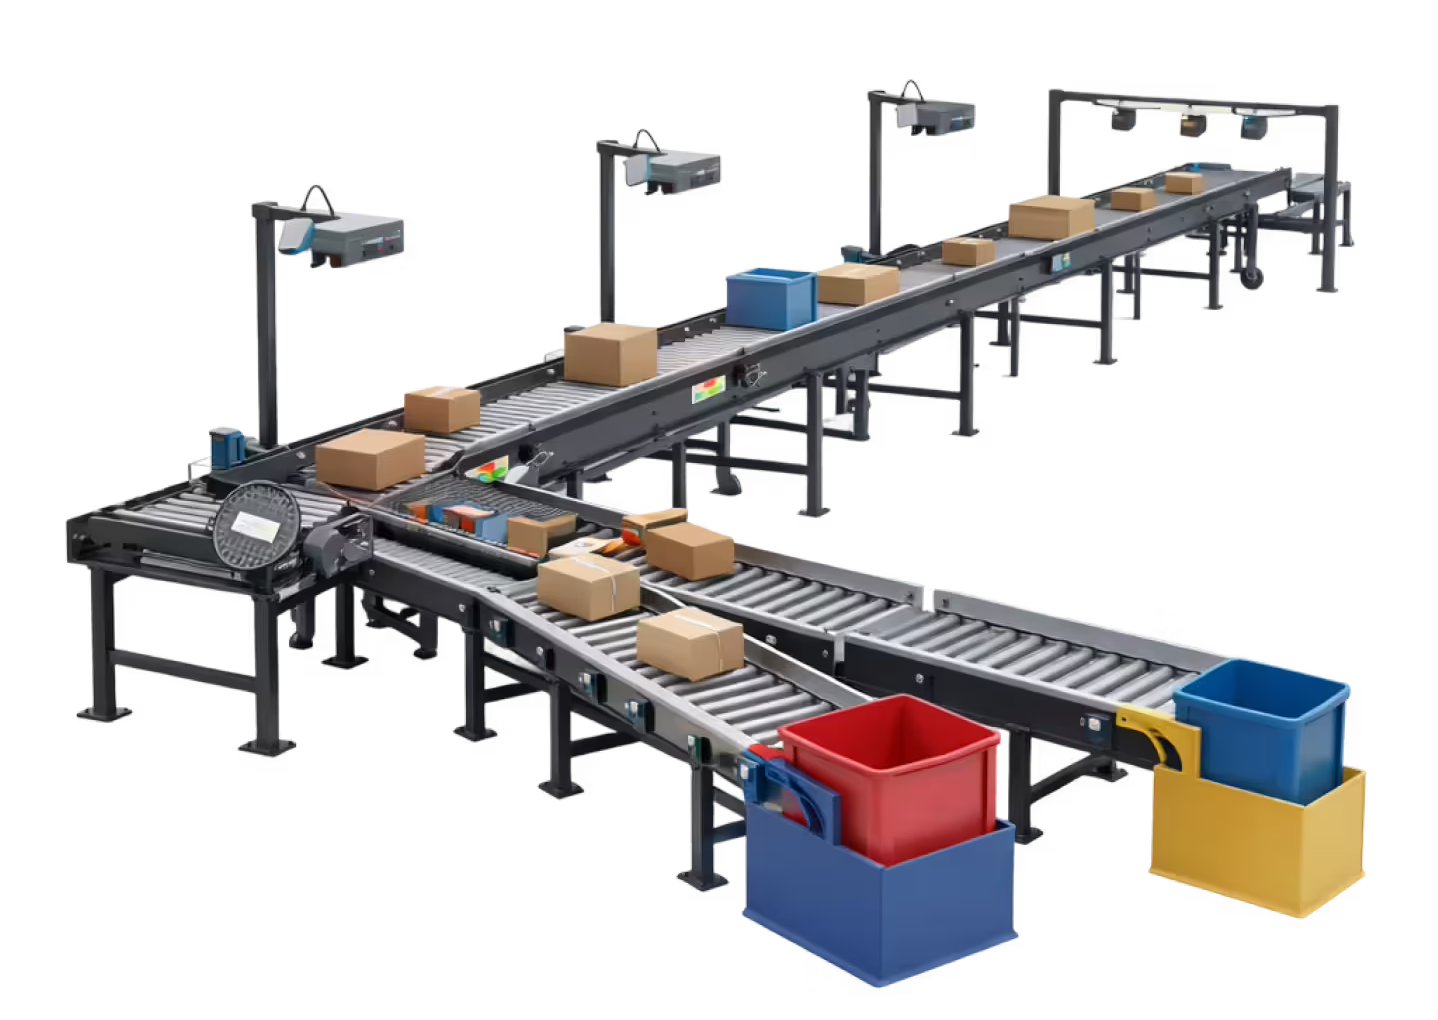
Sortation Conveyor Systems
Sortation conveyors are the brains of a high-volume fulfillment operation. These automated conveyor systems automatically read barcodes or RFID tags and route products to the correct destination — whether that's a shipping lane, packing station, or storage zone. Sortation technologies include shoe sorters, pop-up wheel diverters, tilt-tray sorters, cross-belt sorters, and activated roller belt (ARB) systems.
MWS designs and installs sortation conveyor systems capable of processing thousands of items per hour with near-perfect accuracy, making them essential for operations handling high SKU counts and tight delivery windows.
- Best for: Multi-destination routing, high-volume fulfillment
- Industries: E-Commerce, 3PL, Parcel
- Speed Range: Up to 450 FPM
05
Spiral and Vertical Conveyor Systems
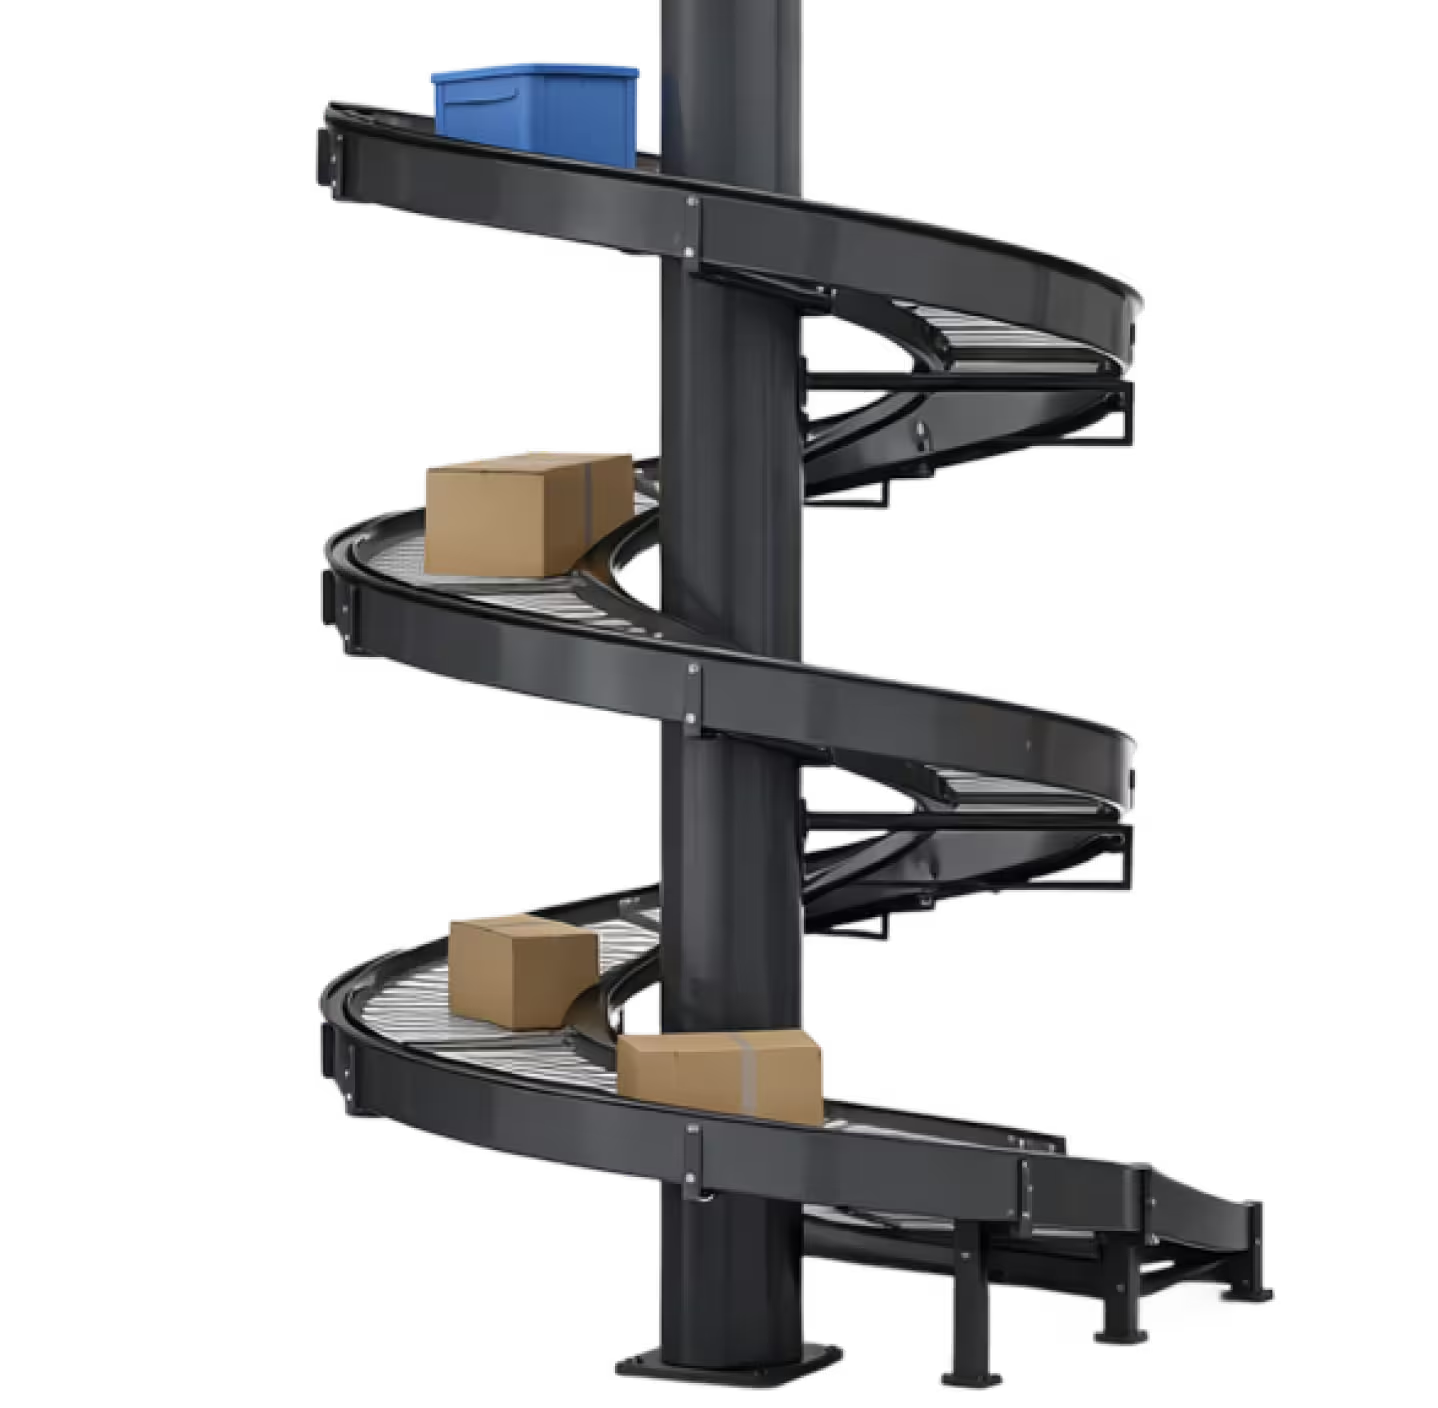
When floor space is limited but you need to move products between levels, spiral and vertical conveyors provide the answer. Spiral conveyors use a continuous helix to gently elevate or lower products — ideal for fragile items and operations that need constant, uninterrupted flow between mezzanine levels, pick modules, or production floors.
Vertical reciprocating conveyors (VRCs) function as freight elevators for automated conveyor systems, lifting pallets, totes, or individual items between levels.
- Best for: Level changes, compact spaces, multi-level warehouses
- Industries: Warehousing, Food and Beverage, Manufacturing
- Speed Range: Up to 200 FPM
06
Pallet Conveyor Systems
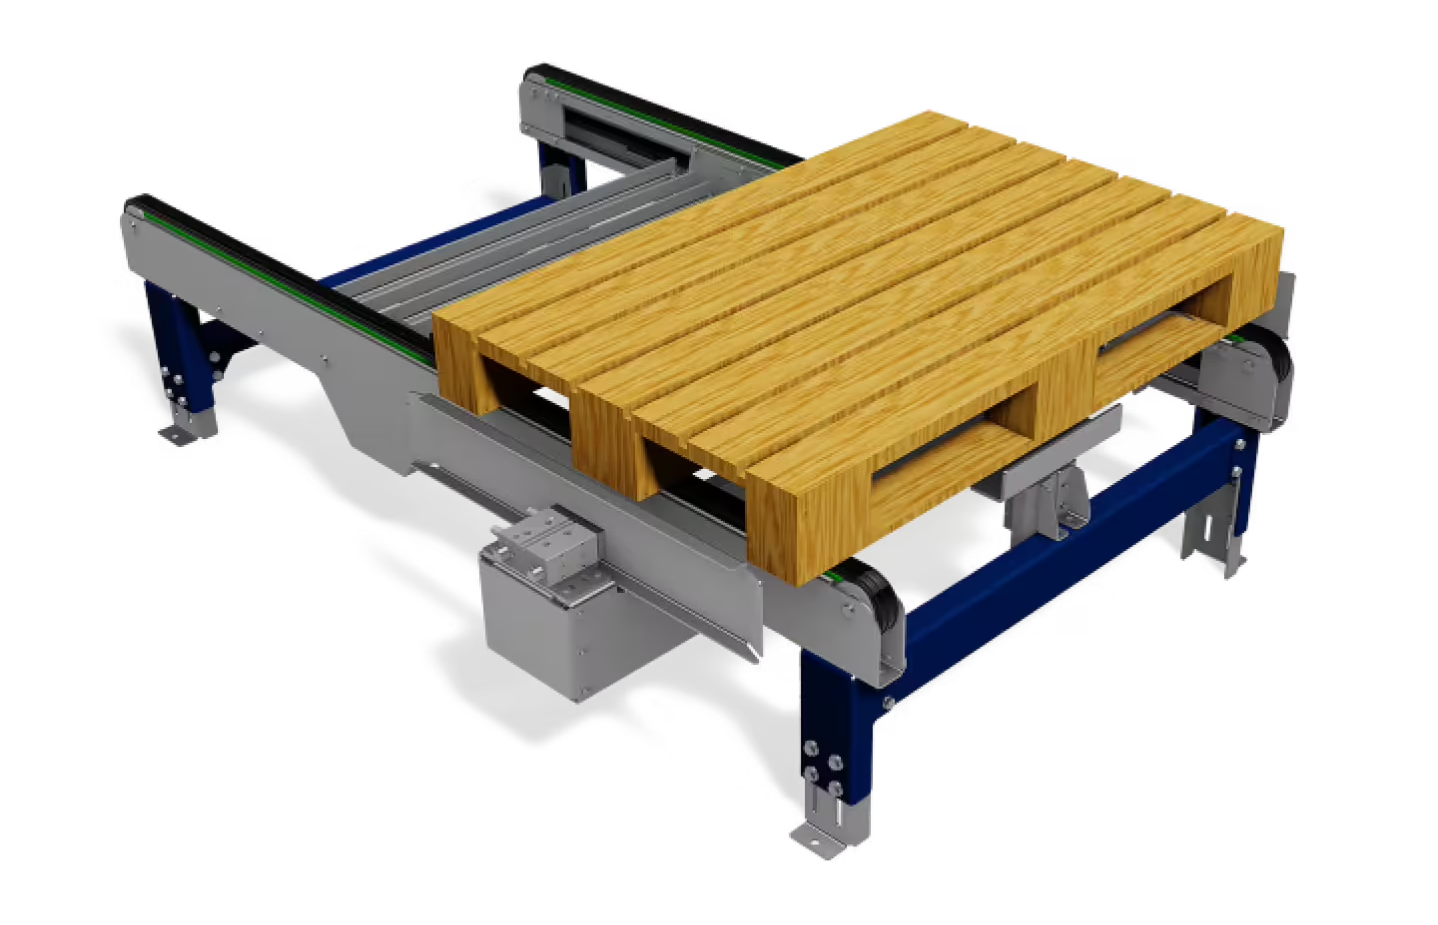
Pallet conveyors are heavy-duty automated conveyor systems designed to handle full pallet loads — typically ranging from 1,000 to 5,000+ pounds. Using chain-driven, roller, or drag-chain technology, these conveyors transport loaded pallets through receiving, storage, picking, and shipping zones with speed and reliability.
MWS integrates pallet conveyors with stretch wrappers, palletizers, and automated storage systems for complete end-to-end pallet handling.
- Best for: Full pallet loads, heavy goods (1,000 to 5,000+ lbs)
- Industries: Manufacturing, Cold Storage, Distribution
- Speed Range: Up to 120 FPM
07
Flexible and Expandable Conveyor Systems
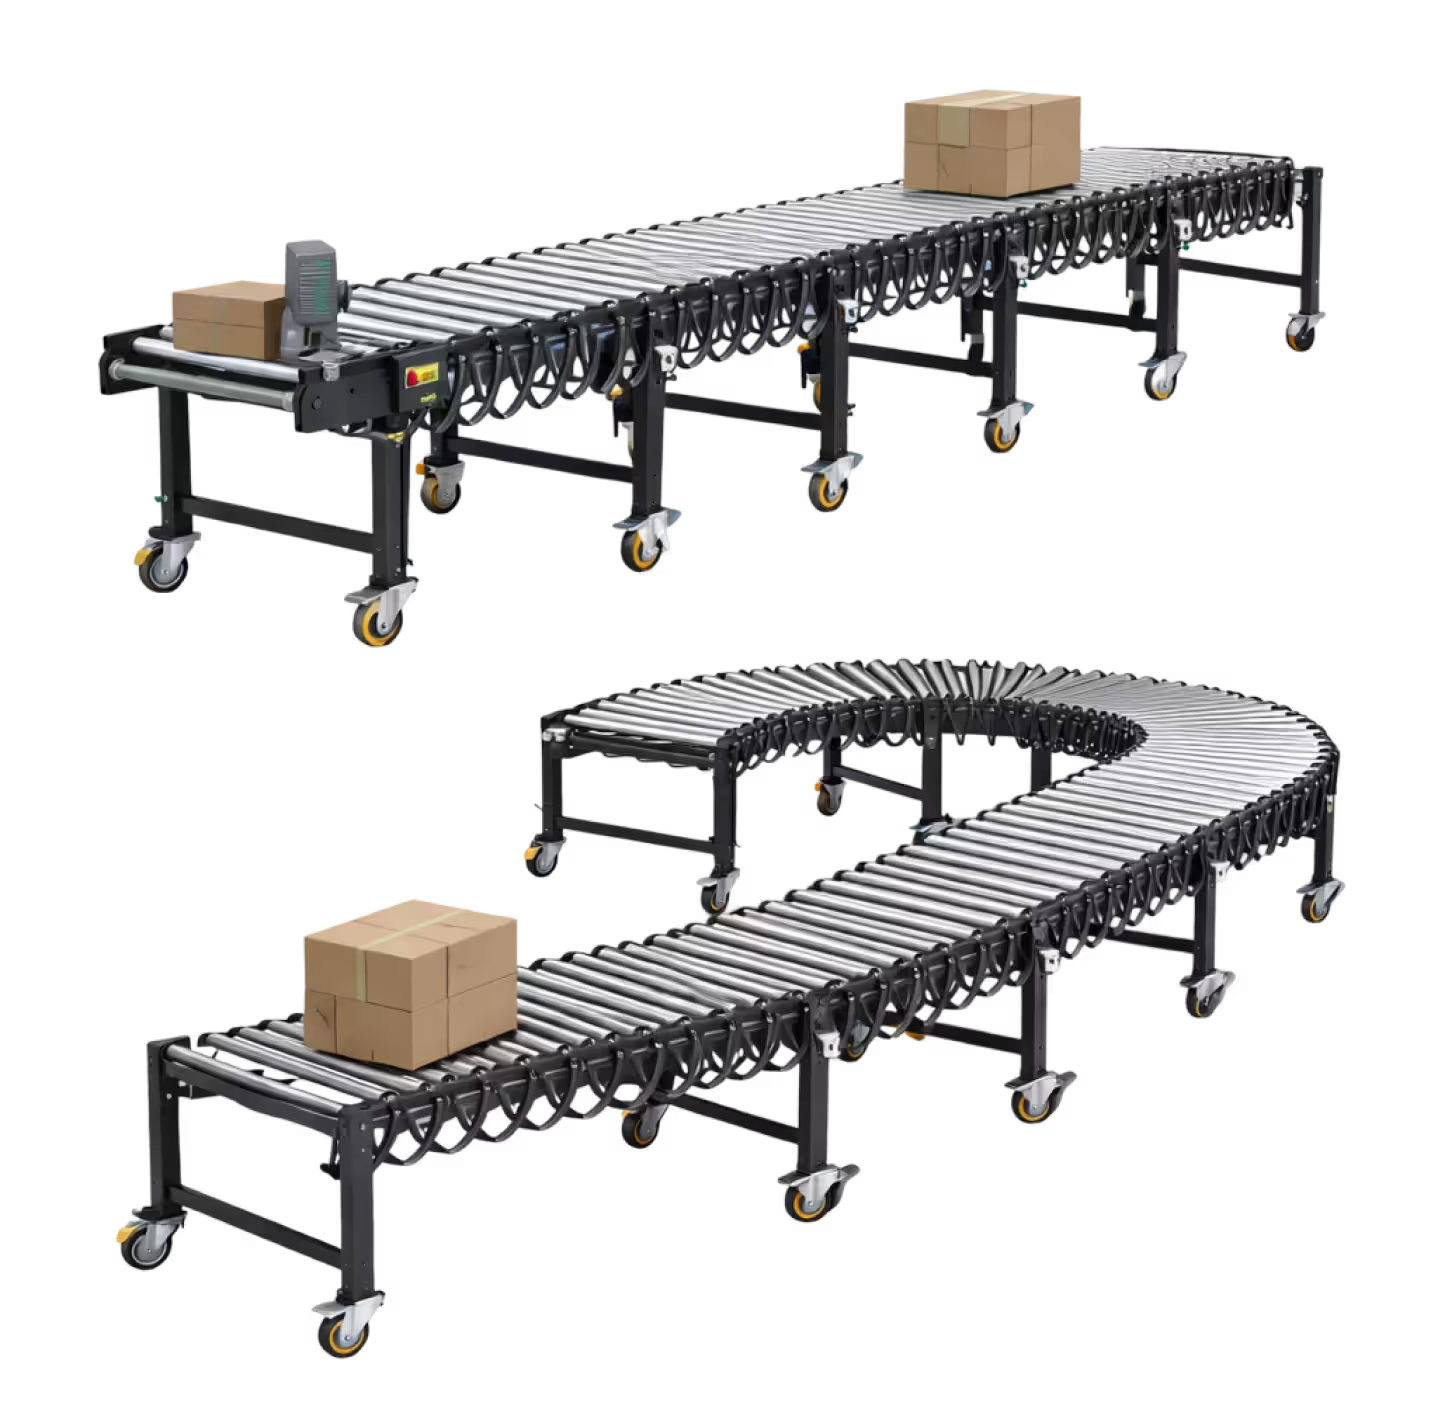
Flexible conveyors are portable, accordion-style conveyor systems that extend, retract, and curve to adapt to changing dock configurations and temporary needs. They are the go-to solution for truck loading and unloading, seasonal surge capacity, and operations that require reconfigurable workflows.
- Best for: Truck loading/unloading, seasonal surge, temporary operations
- Industries: Distribution, Retail, 3PL
- Speed Range: Variable
Key Benefits of Automated
Conveyor Systems
Investing in warehouse conveyor automation delivers compounding returns across labor, throughput, accuracy, and safety — with most automated conveyor systems paying for themselves within 2–3 years.
| Benefit | Impact | Key Data Point |
|---|---|---|
| Increased Throughput | Powers the movement of materials along the conveyor | Electric motors, gear reducers, variable frequency drives (VFDs) |
| Reduced Labor Costs | The surface that carries products from point to point | Belts, rollers, chains, slats, wheels |
| Improved Order Accuracy | Detect, identify, and track products in real time | Functionality |
| Enhanced Worker Safety | Programmable logic that manages routing, speed, and accumulation | Allen-Bradley, Siemens, Omron PLCs |
| Space Optimization | Connects the conveyor to your WMS, ERP, and other automation | OPC-UA, APIs, middleware, SCADA |
| Scalability | Physical support structure for the conveyor system | Steel frames, supports, guards, safety fencing |
Benefit
Increased Throughput
Impact:
Powers the movement of materials along the conveyor
Key Data Point:
Electric motors, gear reducers, variable frequency drives (VFDs)
Reduced Labor Costs
Impact:
The surface that carries products from point to point
Key Data Point:
Belts, rollers, chains, slats, wheels
Improved Order Accuracy
Impact:
Detect, identify, and track products in real time
Key Data Point:
Functionality
Enhanced Worker Safety
Impact:
Programmable logic that manages routing, speed, and accumulation
Key Data Point:
Allen-Bradley, Siemens, Omron PLCs
Space Optimization
Impact:
Connects the conveyor to your WMS, ERP, and other automation
Key Data Point:
OPC-UA, APIs, middleware, SCADA
Scalability
Impact:
Physical support structure for the conveyor system
Key Data Point:
Steel frames, supports, guards, safety fencing
Industries That Use Automated
Conveyor Systems
Automated conveyor systems power operations across a wide range of industries.
If you move products or materials at volume, MWS can help you design and install the right warehouse conveyor system for your operation.
E-Commerce & Retail
The explosive growth of online retail demands automated conveyor systems that can handle massive SKU variety, seasonal surges, and same-day shipping windows. MWS designs fulfillment-grade conveyor systems with integrated sortation and WMS connectivity.
Manufacturing & Assembly
Automated conveyor systems keep manufacturing lines fed with components and raw materials while moving work-in-process between stations. MWS integrates conveyors with robotic cells, palletizers, and quality inspection systems.
Food & Beverage
Food and beverage operations require conveyor systems built with sanitary materials, washdown-rated components, and temperature-tolerant designs. MWS supplies stainless steel, FDA-grade belt conveyors and cold storage systems for the entire food supply chain.
Automotive & Heavy Industry
The automotive industry relies on pallet conveyors and heavy-duty roller systems to move engine blocks, stamped panels, and subassemblies between workstations. MWS builds automated conveyor systems engineered for extreme weight and continuous duty cycles.
Cold Storage & Frozen Goods
Specialized cold storage conveyor systems minimize worker exposure to hazardous freezer environments while maintaining product integrity through the cold chain. MWS uses cold-rated motors, stainless steel frames, and low-temperature lubricants.
3PL & Logistics
Third-party logistics providers need automated conveyor systems that can adapt to multiple clients, changing product mixes, and seasonal volume spikes. MWS designs modular, reconfigurable warehouse conveyor systems that scale with your business.
How to Choose the Right
Automated Conveyor System
Selecting the right automated conveyor system is one of the most important decisions you'll make for your warehouse operation. Here's a structured framework to guide your evaluation
- Size and weight: Determines belt width, roller spacing, and motor power
- Shape: Flat-bottomed items suit rollers; irregular shapes need belts
- Fragility: Delicate items require accumulation zones and gentle transitions
- Packaging: Polybags, loose items, and small parts need belt conveyors; rigid cartons work on rollers
- Most automated conveyor systems deliver full ROI in 2–3 years
- Phased approaches let you start smaller and expand as savings compound
- Higher upfront investment in sortation and WMS integration typically yields the fastest payback
- MWS provides transparent pricing and custom ROI analysis at no cost
- Low volume (under 1,000/hr) — Simple powered conveyors may suffice
- Medium volume (4,000–8,000/hr) — Powered conveyors with basic accumulation and sortation
- High volume (10,000–100,000+/hr) — Multi-zone sortation, high-speed belts, and full automation
- Your automated conveyor system speed, width, and number of lines all flow from this number
- Modular conveyor system design allows adding zones, lines, and automation layers
- Building in expansion capacity upfront costs less than retrofitting later
- Consider 3–5 year growth projections when sizing your system
- Available floor space, ceiling height, and column locations constrain system routing
- Dock door positions and traffic patterns affect conveyor entry/exit points
- Mezzanine or multi-level operations may require spiral or vertical conveyors
- Existing equipment and workflows must be integrated, not disrupted
- Cold storage: Requires cold-rated motors, bearings, and lubricants (-20°F to -40°F)
- Washdown / sanitary: Stainless steel, FDA-grade belts, IP-rated components
- Cleanroom: Particle-controlled environments with specialized materials
- Outdoor / harsh: Weather-resistant and dust-tight enclosures
- WMS / ERP: SAP, Oracle, Manhattan, Blue Yonder, Körber, HighJump
- Automation equipment: Robotic picking, AS/RS, print-and-apply, palletizers
- Scanning / vision: Barcode readers, RFID, dimensioners, vision systems
- Your conveyor system's PLC must communicate with all of these in real time
- Simple single-line installs: 1–3 weeks
- Mid-sized systems: 15 weeks
- Large sortation networks: 6–8 months
- Total project (design through commissioning):4–12 months
Pro tip: The most reliable way to choose the right automated conveyor system is to work with an experienced conveyor system integrator like MWS. We evaluate all of these factors during our free consultation and recommend a system tailored to your exact needs.
Not Sure Which Conveyor Type
Is Right for Your Operation?
Talk to a conveyor specialist who can evaluate your needs and recommend the best solution for your facility.
Or call us at 515-635-1555
Key Factors That Affect
Conveyor System Cost
Understanding what drives price helps you budget accurately and avoid surprises. Here are the key factors that affect your total automated conveyor system investment:
Total System Length
More linear feet means a higher total cost, but cost per foot typically decreases at scale. A 500-foot belt mainline will cost significantly more than a 100-foot workstation feed, but delivers greater efficiency gains.
Conveyor Type
Sortation and spiral systems carry the highest per-foot costs ($1,000–$5,000+/ft), while gravity conveyors are the most economical ($100–$300/ft). Your mix of conveyor types has a major impact on total project cost.
Automation Level
The more sensors, PLCs, VFDs, and software integration your system requires, the higher the cost. A basic powered roller line is far less expensive than a fully WMS-integrated sortation network with real-time tracking.
Controls & Software
PLC programming, WMS integration, HMI touchscreen panels, and SCADA monitoring can add $20,000 to $200,000+ to your project, depending on complexity and the number of integration points.
Installation Complexity
Mezzanine integration, structural reinforcement, electrical upgrades, and phased installations (to minimize operational disruption) all increase labor and project management costs.
Ongoing Maintenance
Preventive maintenance contracts range from $5,000 to $50,000+ per year depending on system size, but they protect your investment and prevent costly unplanned downtime.
Manufacturer & Brand
Premium manufacturers like Hytrol, Dematic, Interroll, and TGW command higher prices but offer longer warranties, better parts availability, and proven reliability.
The bottom line: A complete automated conveyor system for a mid-sized distribution center typically ranges from $500,000 to $5 million+ depending on scope, complexity, and automation level. The best approach is to contact an automated conveyor systems supplier like MWS for a free consultation and custom quote
Our Proven 6-Step Automated Conveyor System Process
From initial assessment to ongoing support, our structured process ensures your automated conveyor system is designed right, installed right, and performs right — every time. This is what sets MWS apart as a trusted conveyor system integrator.
01
Consultation and Data Collection
Our team visits your facility to evaluate current operations, throughput requirements, product types, space constraints, and growth plans.
We document every detail to ensure the automated conveyor system we design fits your exact needs — at no cost and no obligation.
WEEK 1-3
02
Mechanical System, Layout
and Controls
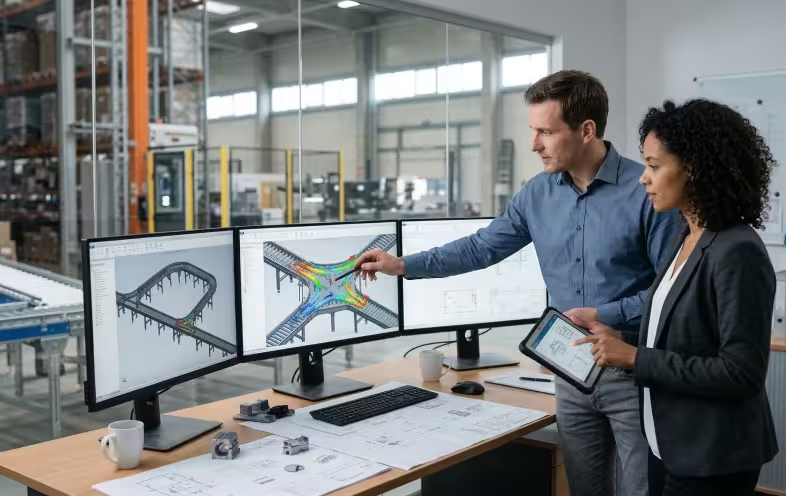
Our engineers create a custom conveyor system layout using CAD modeling and simulation software.
We optimize for maximum efficiency, considering traffic flow, integration points, and future scalability — so your warehouse conveyor system works today and grows with you tomorrow.
WEEK 3-5
03
Equipment Proposal and Purchasing
We source the best conveyor equipment from our network of top manufacturers, including Hytrol, Dematic, Interroll, and others.
As a trusted conveyor system integrator, we leverage volume relationships to deliver premium components at competitive pricing.
WEEK 6-8
04
Conveyor and
Controls Production
Our certified installation crews handle every aspect of the build-out — structural steel, electrical, controls, and software integration. We minimize disruption to your ongoing warehouse operations with phased installation plans.
WEEK 9-20
05
Conveyor and Controls
Installation and Start up
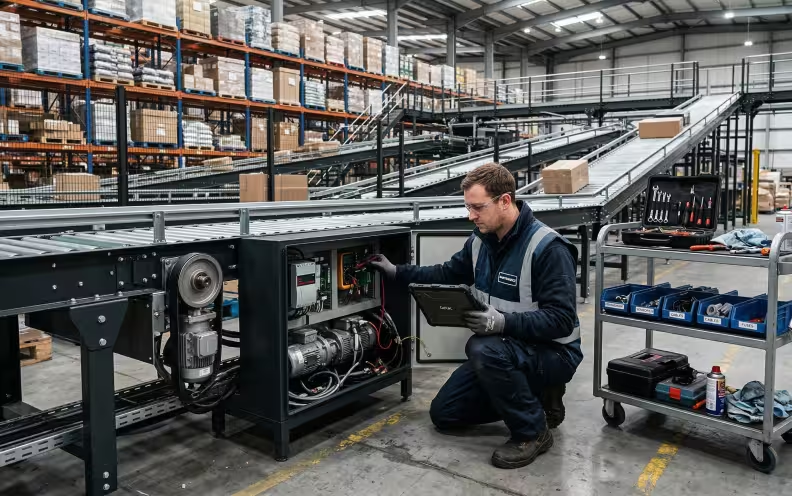
Every automated conveyor system undergoes rigorous testing. We commission all controls, run product through every path, verify sort accuracy, and train your team on operations, safety procedures, and basic troubleshooting.
WEEK 20-26
06
Ongoing
maintenance and support
Our relationship doesn't end at installation. We offer preventive maintenance programs, emergency service, spare parts inventory, and conveyor system optimization reviews to keep your automated conveyors at peak performance year after year.
ONGOING
Why Choose MWS as Your Automated
Conveyor Systems Supplier
We don't just sell conveyor equipment — we design, engineer, install, and support complete automated conveyor systems. That's the integrator difference, and it's why operations across the Midwest trust MWS.
| Capability | MWS (Full-Service Integrator) | Equipment-Only Dealer | General Contractor |
|---|---|---|---|
| Custom System Design & Engineering | ✓In-house CAD & simulation |
✕Limited or outsourced |
✕Not offered |
| Equipment Procurement (Multi-Brand) | ✓Access to all top manufacturers |
✓Access to all top manufacturers |
✕Relies on subcontractors |
| Professional Installation | ✓Own certified crews |
✕Subcontracted or DIY |
✓General install only |
| Controls and PLC- MWS partners with Lafayette Engineering | ✓In-house controls engineering |
✕Third-party required |
✕Third-party required |
| WMS/ERP- Partners with Lafayette engineering | ✓Full software integration |
✕Not offered |
✕Not offered |
| Commissioning & Training | ✓Rigorous testing + operator training |
✕Basic startup only |
✕Not offered |
| Ongoing Maintenance & Support | ✓Preventive + emergency service |
✕Warranty only |
✕Not offered |
| Single Point of Accountability | ✓One partner, one team |
✕Multiple vendors to manage |
✕Finger-pointing between trades |
| 50+ Years of Warehouse Expertise | ✓Since 1979 |
!Varies |
✕Not warehouse-specific |
Capability
Custom System Design & Engineering
| MWS (Full-Service Integrator) | ✓In-house CAD & simulation |
| Equipment-Only Dealer | ✕Limited or outsourced |
| General Contractor | ✕Not Offered |
Equipment Procurement (Multi-Brand)
| MWS (Full-Service Integrator) | ✓Access to all top manufacturers |
| Equipment-Only Dealer | ✓Access to all top manufacturers |
| General Contractor | ✕Relies on subcontractors |
Professional Installation
| MWS (Full-Service Integrator) | ✓Own certified crews |
| Equipment-Only Dealer | ✕Subcontracted or DIY |
| General Contractor | ✓General install only |
Controls and PLC- MWS partners with Lafayette Engineering
| MWS (Full-Service Integrator) | ✓In-house controls engineering |
| Equipment-Only Dealer | ✕Third-party required |
| General Contractor | ✕Third-party required |
WMS/ERP- Partners with Lafayette engineering
| MWS (Full-Service Integrator) | ✓Full software integration |
| Equipment-Only Dealer | ✕Not offered |
| General Contractor | ✕Not offered |
Commissioning & Training
| MWS (Full-Service Integrator) | ✓Rigorous testing + operator training |
| Equipment-Only Dealer | ✕Basic startup only |
| General Contractor | ✕Not offered |
Ongoing Maintenance & Support
| MWS (Full-Service Integrator) | ✓Preventive + emergency service |
| Equipment-Only Dealer | ✕Warranty only |
| General Contractor | ✕Not offered |
Single Point of Accountability
| MWS (Full-Service Integrator) | ✓One partner, one team |
| Equipment-Only Dealer | ✕Multiple vendors to manage |
| General Contractor | ✕Finger-pointing between trades |
50+ Years of Warehouse Expertise
| MWS (Full-Service Integrator) | ✓Since 1979 |
| Equipment-Only Dealer | !Varies |
| General Contractor | ✕Not warehouse-specific |
Integrator-Led Approach
MWS manages every phase — from initial assessment and CAD-engineered conveyor system design to equipment procurement, professional installation, and commissioning. One partner. One accountable team. One automated conveyor system that works.
50+ Years of Warehouse Expertise
Founded in 1979, MWS brings over five decades of warehouse equipment and conveyor automation experience. We've designed and installed automated conveyor systems for operations of every size — and we know what works.
Top Manufacturer Partnerships
We partner with the industry's leading conveyor manufacturers, giving you access to premium conveyor equipment at competitive pricing — backed by factory warranties and our own service support.
Turnkey Automated Conveyor Solutions
From the first site visit to the final commissioning walkthrough and operator training — we handle your entire automated conveyor system project. You focus on running your business; we focus on building your system right.
Midwest Service Coverage
Based in Iowa and serving warehouse conveyor system installations across Iowa, Illinois, Indiana, Michigan, Minnesota, Missouri, Ohio, Wisconsin, Kansas, Nebraska, and the Dakotas — with service teams that respond fast.
Single-Source Accountability
No finger-pointing between equipment vendors, electricians, and software providers. MWS is your single point of contact and accountability for your entire automated conveyor system project.
Ready to Work with a Trusted Automated
Conveyor Systems Supplier?
Over 50 years of experience. Turnkey design, installation, and support. One partner, one accountable team. Let's build your system.
Or call us at 515-635-1555
Frequently Asked Questions
About Automated Conveyor Systems
Get answers to the most common questions about automated conveyor systems, costs, installation timelines, and maintenance. These are the questions warehouse managers, operations directors, and facility planners ask most.
How much do automated conveyor systems cost?
Automated conveyor system costs vary significantly based on system complexity, total length, conveyor type, automation level, controls, software integration, and facility-specific requirements. As a general range: simple gravity roller conveyors may cost $100–$300 per linear foot; powered belt conveyors typically range from $300–$800 per linear foot; and advanced sortation systems with controls and WMS integration can range from $1,000–$3,000+ per linear foot. A complete automated conveyor system for a mid-sized distribution center typically represents a total investment of $500,000 to $5 million or more, depending on scope. The best approach is to contact an automated conveyor systems supplier like Midwest Warehouse Solutions for a free consultation and custom quote tailored to your specific throughput requirements, product types, and facility layout. Call 515-635-1555 for a no-obligation estimate.
How do I choose the right automated conveyor system for my operation?
Choosing the right automated conveyor system requires a careful evaluation of several factors: Product characteristics — size, weight, shape, fragility, and packaging type determine which conveyor surface and drive mechanism is appropriate. Throughput requirements — how many units per hour you need to process dictates system speed, width, and complexity. Facility layout — available floor space, ceiling height, column locations, dock door positions, and existing equipment all constrain and inform design. Integration needs — compatibility with your WMS, ERP, and other warehouse automation systems is essential for a coordinated operation. Budget and ROI timeline — balancing initial capital investment against projected operational savings helps determine the right level of automation. Scalability — your conveyor system should accommodate future growth without requiring a complete rebuild. Environmental conditions — temperature, humidity, and cleanliness requirements affect material selection. Working with an experienced conveyor system integrator like MWS is the most reliable way to match the right system to your specific operation.
What is the ROI on automated conveyor systems?
Most automated conveyor systems deliver full return on investment within 2–3 years through a combination of measurable savings: Labor cost reduction — typically 30–40% fewer material handling staff needed, redirecting headcount to higher-value tasks. Throughput gains — 2–3x more orders fulfilled per hour compared to manual operations. Accuracy improvements — up to 99.9% order accuracy, dramatically reducing costly errors, returns, and customer dissatisfaction. Safety improvements — fewer workplace injuries from manual lifting and repetitive motion, reducing workers' compensation costs. Lower long-term operating costs — automated conveyors operate consistently without overtime, benefits, or turnover costs. Many MWS clients see payback in under 24 months, with ongoing annual savings of $200,000 to $1 million or more in labor and operational costs, depending on the scale of the operation.
Do automated conveyor systems integrate with WMS and ERP software?
Yes. Modern automated conveyor systems are designed to integrate seamlessly with all major warehouse management systems, including SAP, Oracle WMS, Manhattan Associates, Blue Yonder, Körber, HighJump, and many others. Integration is achieved through standardized communication protocols (such as OPC-UA), APIs, and middleware layers. The conveyor system's programmable logic controllers (PLCs) communicate with your WMS to receive real-time routing instructions, update inventory positions, confirm sortation accuracy, and coordinate with other automated equipment such as robotic picking systems, automated storage and retrieval systems (AS/RS), print-and-apply labelers, and shipping sorters. Midwest Warehouse Solutions handles all WMS integration as part of our turnkey conveyor system installation service, working directly with your WMS provider to ensure seamless data flow from day one.
What maintenance do automated conveyor systems require?
Regular preventive maintenance is essential for optimal conveyor system performance and longevity. Key maintenance activities include: Daily — visual inspections, debris removal, and listening for unusual noises. Weekly — belt tracking and tension checks, roller inspection, and emergency stop testing. Monthly — lubrication of bearings, chains, and moving parts; sensor cleaning; and drive component inspection. Quarterly — electrical connection inspections, sensor calibration, software updates, and safety system verification. Annually — comprehensive conveyor system audits including motor testing, structural inspection, controls review, and performance benchmarking. Modern IoT-enabled automated conveyor systems also support predictive maintenance, using real-time sensor data to monitor vibration, temperature, amperage, and power consumption — identifying potential failures before they cause unplanned downtime. MWS offers comprehensive preventive and predictive maintenance programs tailored to your specific automated conveyor system.
Can automated conveyor systems work in cold storage and freezer environments?
Yes. Specialized automated conveyor systems are available for cold storage and freezer environments operating at temperatures as low as -20°F to -40°F. These systems use cold-rated components including stainless steel frames, low-temperature lubricants, sealed bearings, and motors rated for sub-zero operation. Cold storage conveyor systems reduce the time workers spend in hazardous freezer environments, improve throughput in temperature-sensitive supply chains, and maintain product integrity throughout the cold chain. MWS designs and installs cold storage conveyor systems for food and beverage, pharmaceutical, and frozen goods operations.
How do automated conveyor systems improve warehouse safety?
Automated conveyor systems significantly improve warehouse safety by eliminating the most common causes of workplace injuries: manual lifting, carrying heavy loads, repetitive motion, and forklift traffic. By automating product transport, warehouse conveyor systems reduce the physical strain on workers, decrease forklift traffic in pedestrian areas, and minimize the risk of product drops and collisions. Many operations see a 50%+ reduction in material handling injuries after installing automated conveyors. Additionally, modern systems include safety features like emergency stop pull cords, guard rails, light curtains, and automated lockout/tagout capabilities.
Plan Your Project
with Our Team
Free consultation
Request a Free Automated
Conveyor System Quote
Tell us about your operation and our team will design a custom automated conveyor system tailored to your requirements. No obligation. Fast response. 50+ years of expertise behind every recommendation.
Or call us at 515-635-1555
Save time. We will contact you
Provide your details, and we’ll help you find exactly what you need